Yongkang, Zhejiang · Aluminium castings for diesel engines
Aluminium in,
engine-ready parts out
Gravity and high-pressure die casting for cylinder heads, bearing caps, intake manifolds, EGR valve seats, valve covers, gear chambers and oil pans. Melting, core making, casting, T6 heat treatment, machining and inspection all run inside our own plant.
Company
Twenty years on one category: aluminium engine parts
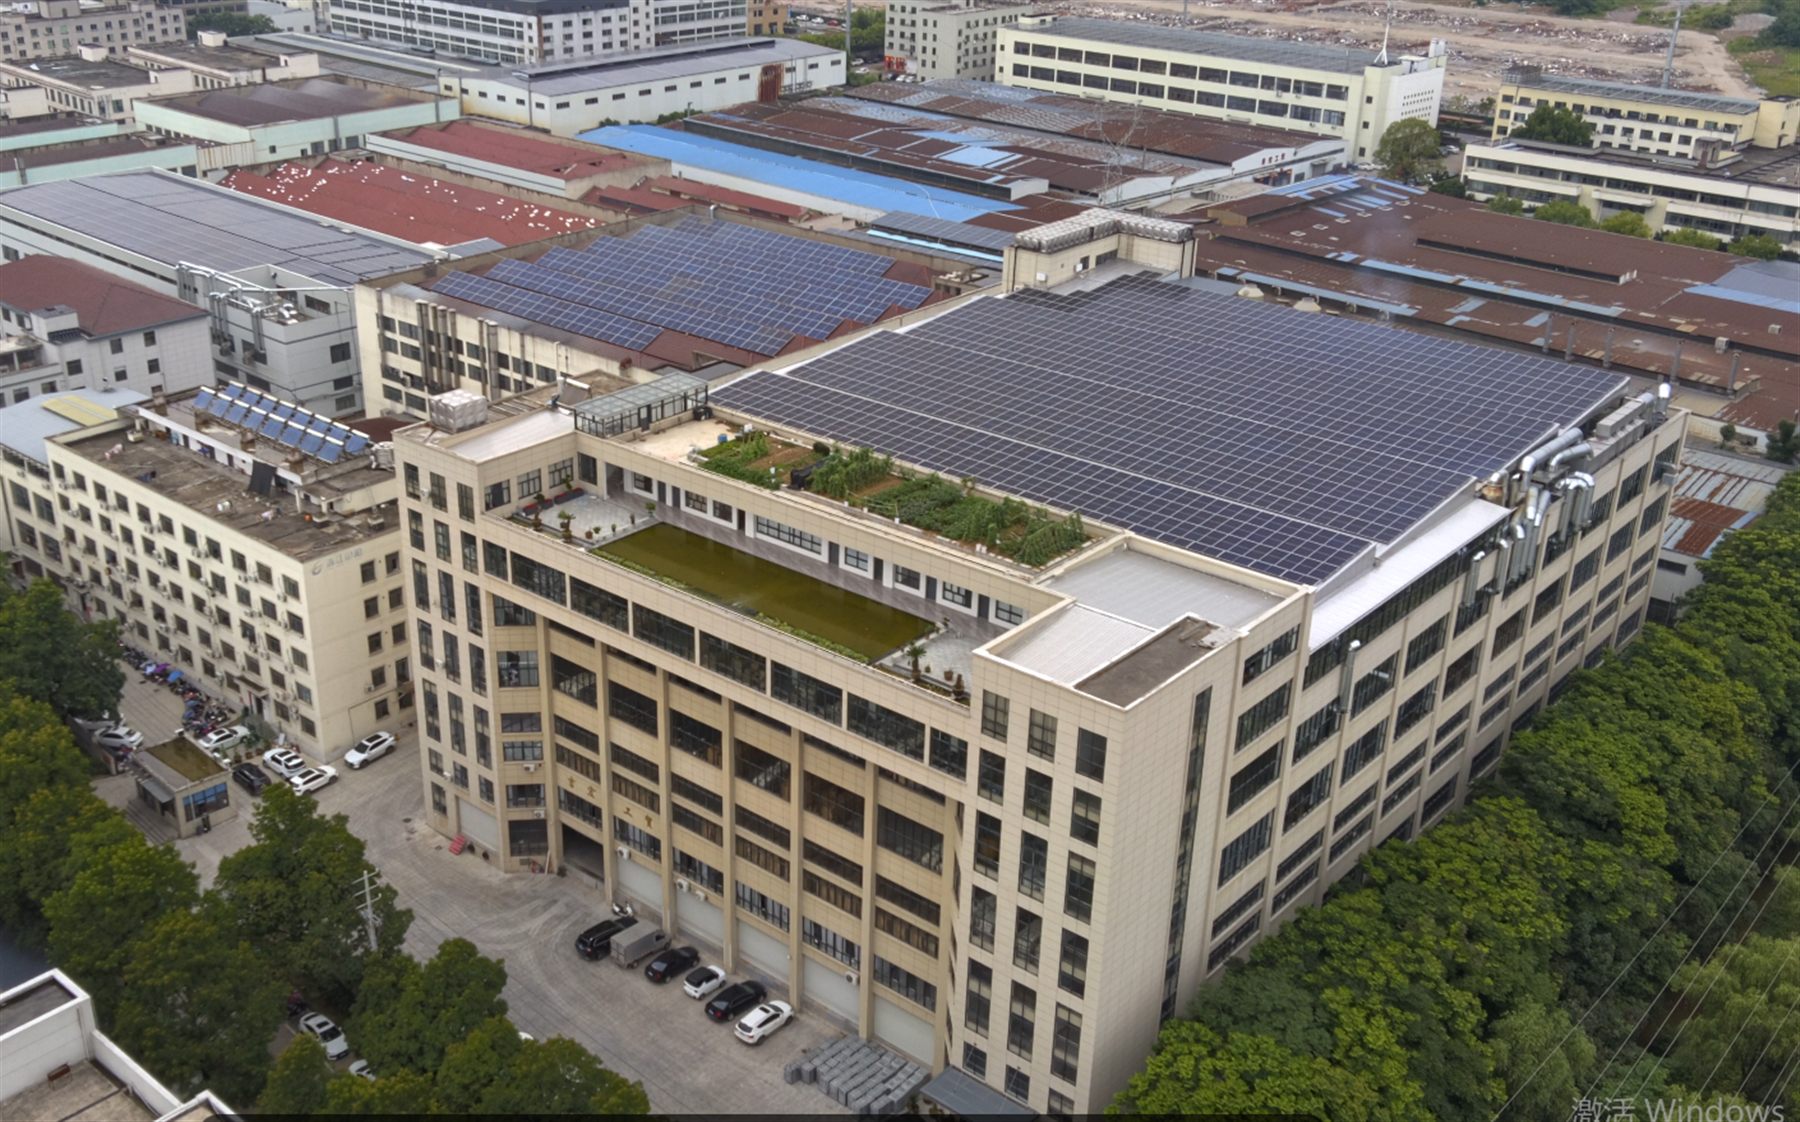
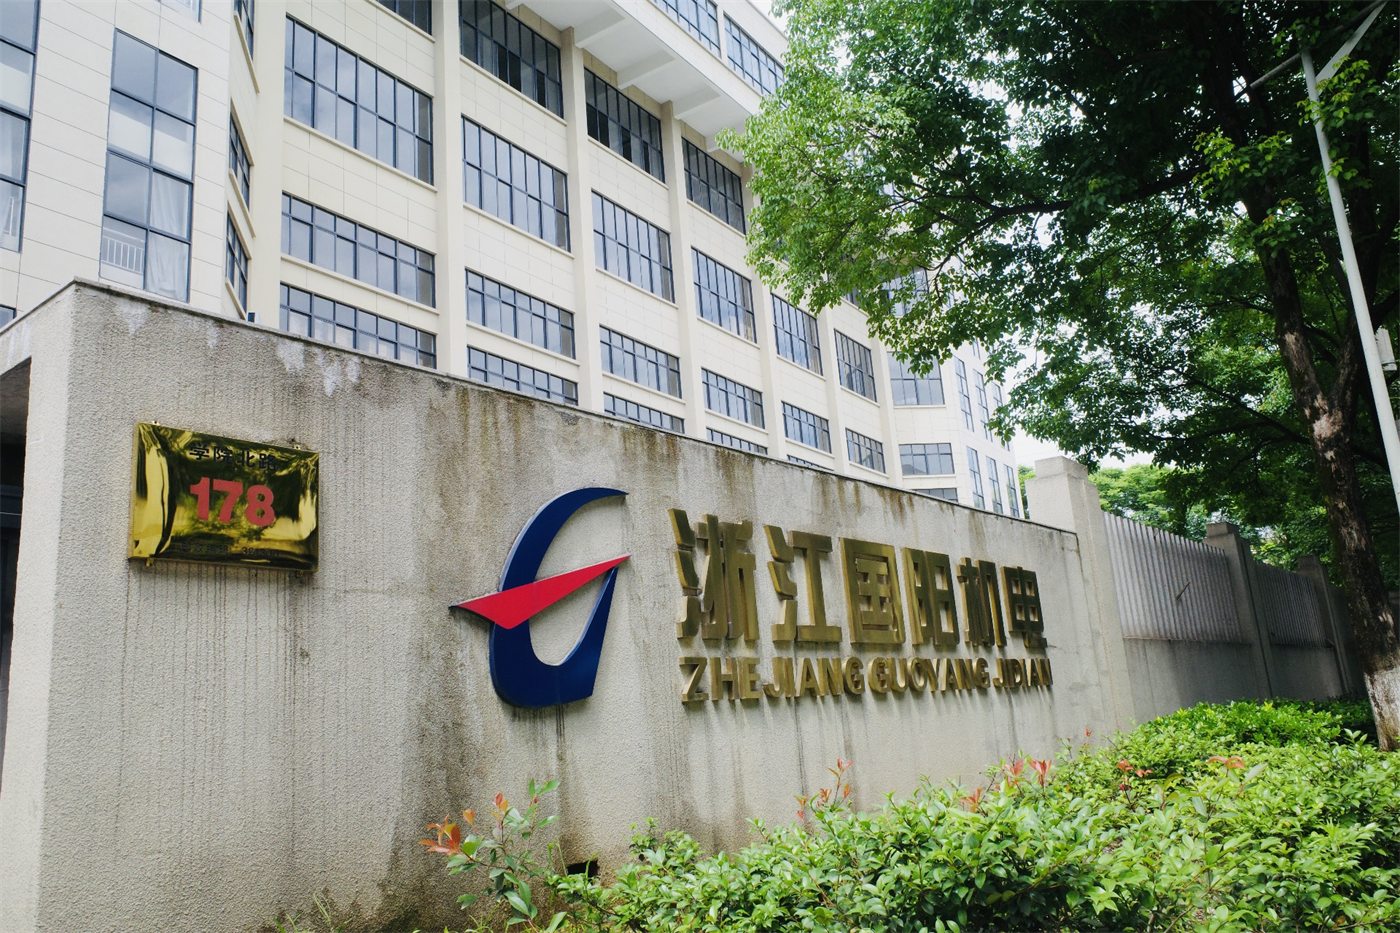
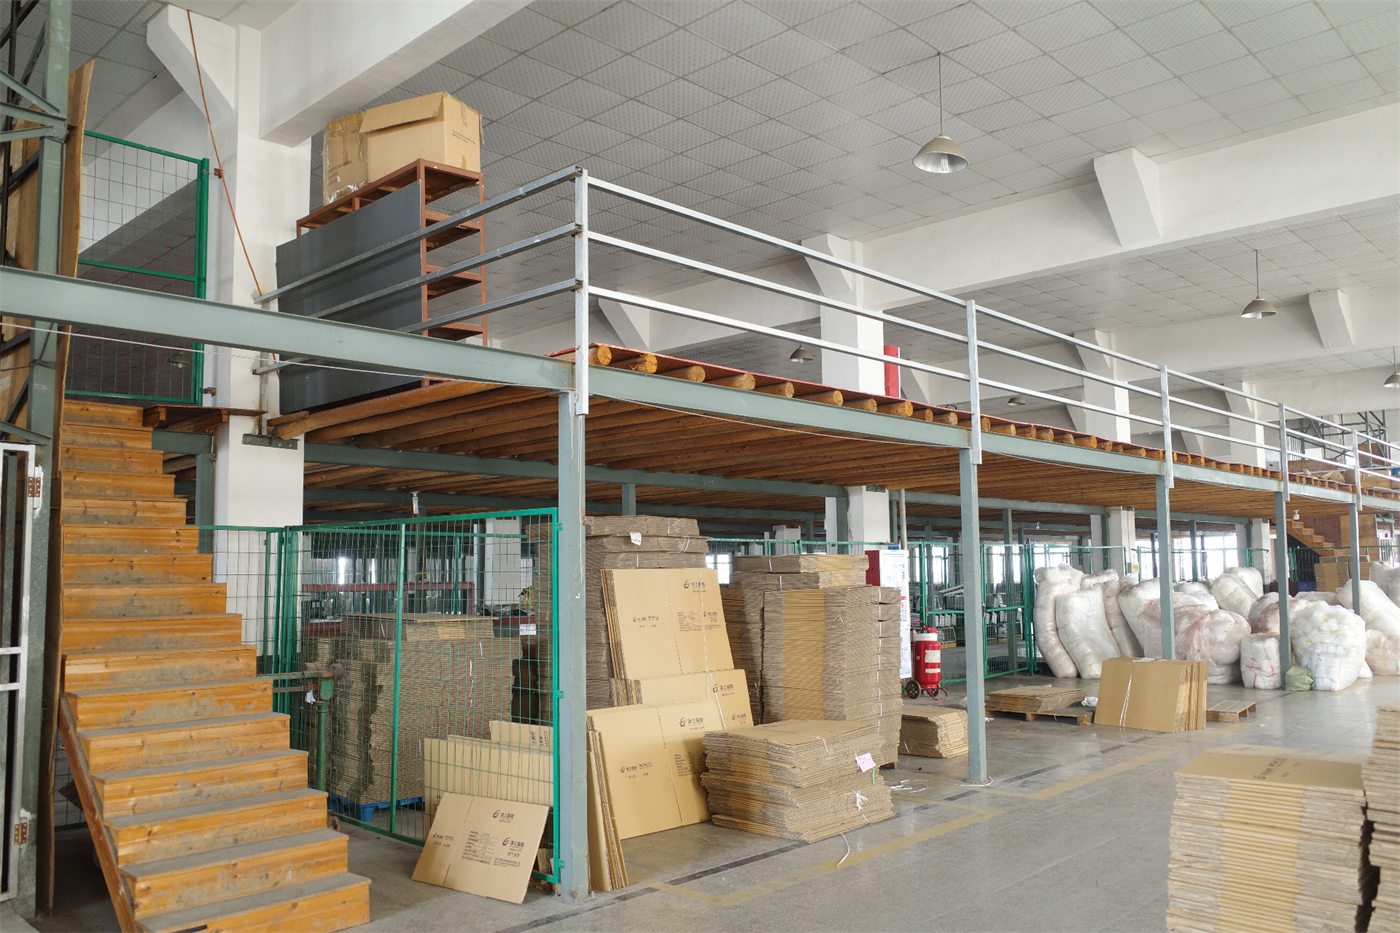
Guoyang began as Yongkang Guoyang Aluminum Co., Ltd. and was incorporated as Zhejiang Guoyang Electromechanical Manufacturing Co., Ltd. on 6 December 2004. The plant at 178 Xueyuan North Road in the Yongkang Economic Development Zone covers a 30,000 m² site with more than 60,000 m² of factory floor space; the 25,049 m² No. 3 plant was completed in 2022. We employ more than 260 people and reported sales of RMB 125 million in 2025.
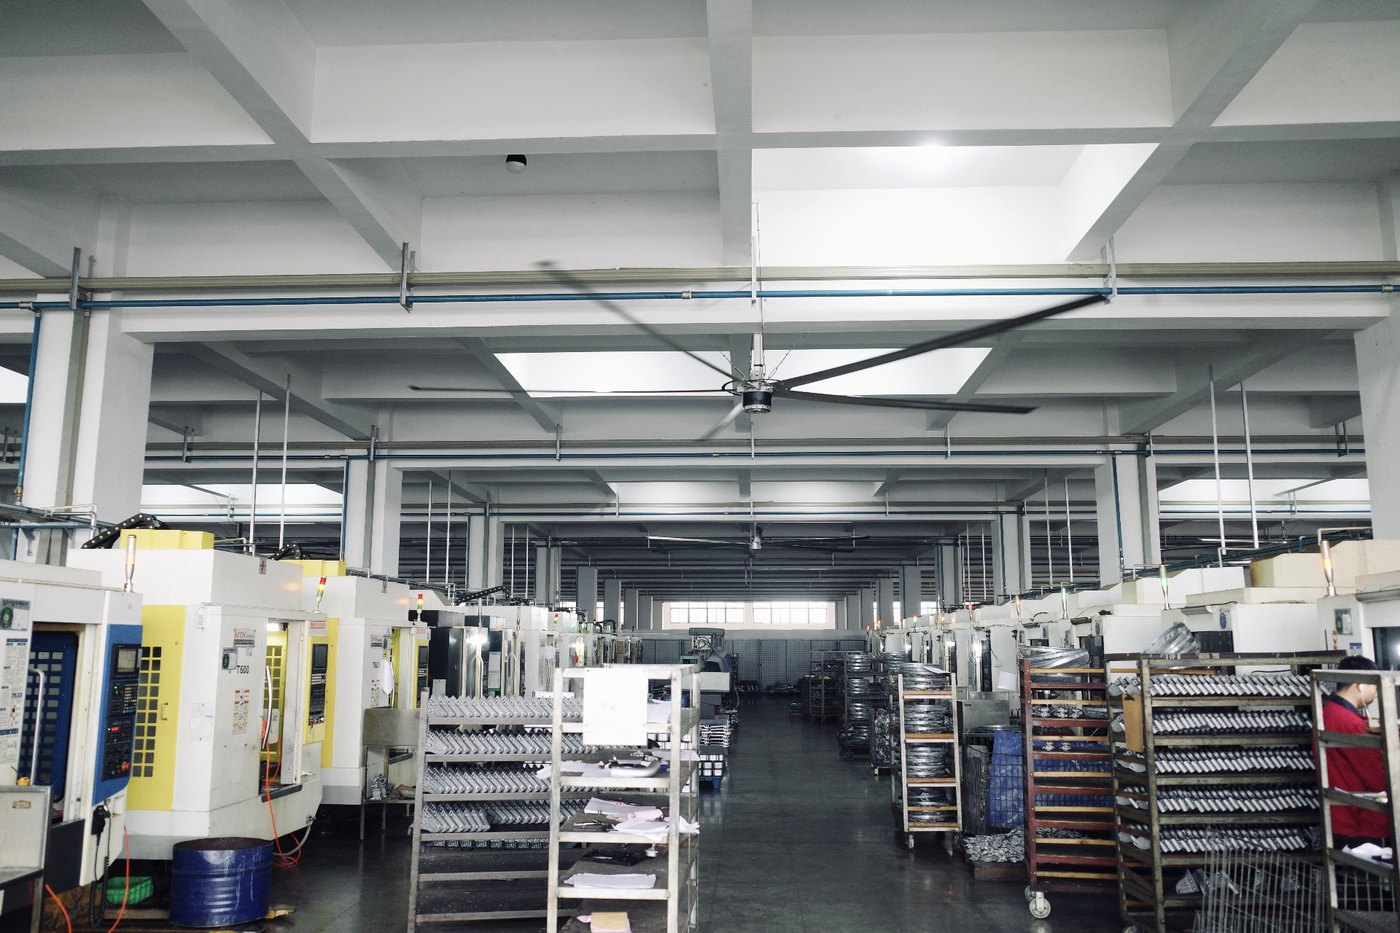
For more than twenty years we have done one thing: turn aluminium into parts that bolt straight onto an engine. Billet melting, sand cores, gravity and high-pressure casting, T6 heat treatment, precision machining and final inspection are all in-house. Moulds and fixtures are designed and built here too, so a customer revision never waits for an outside tool shop.
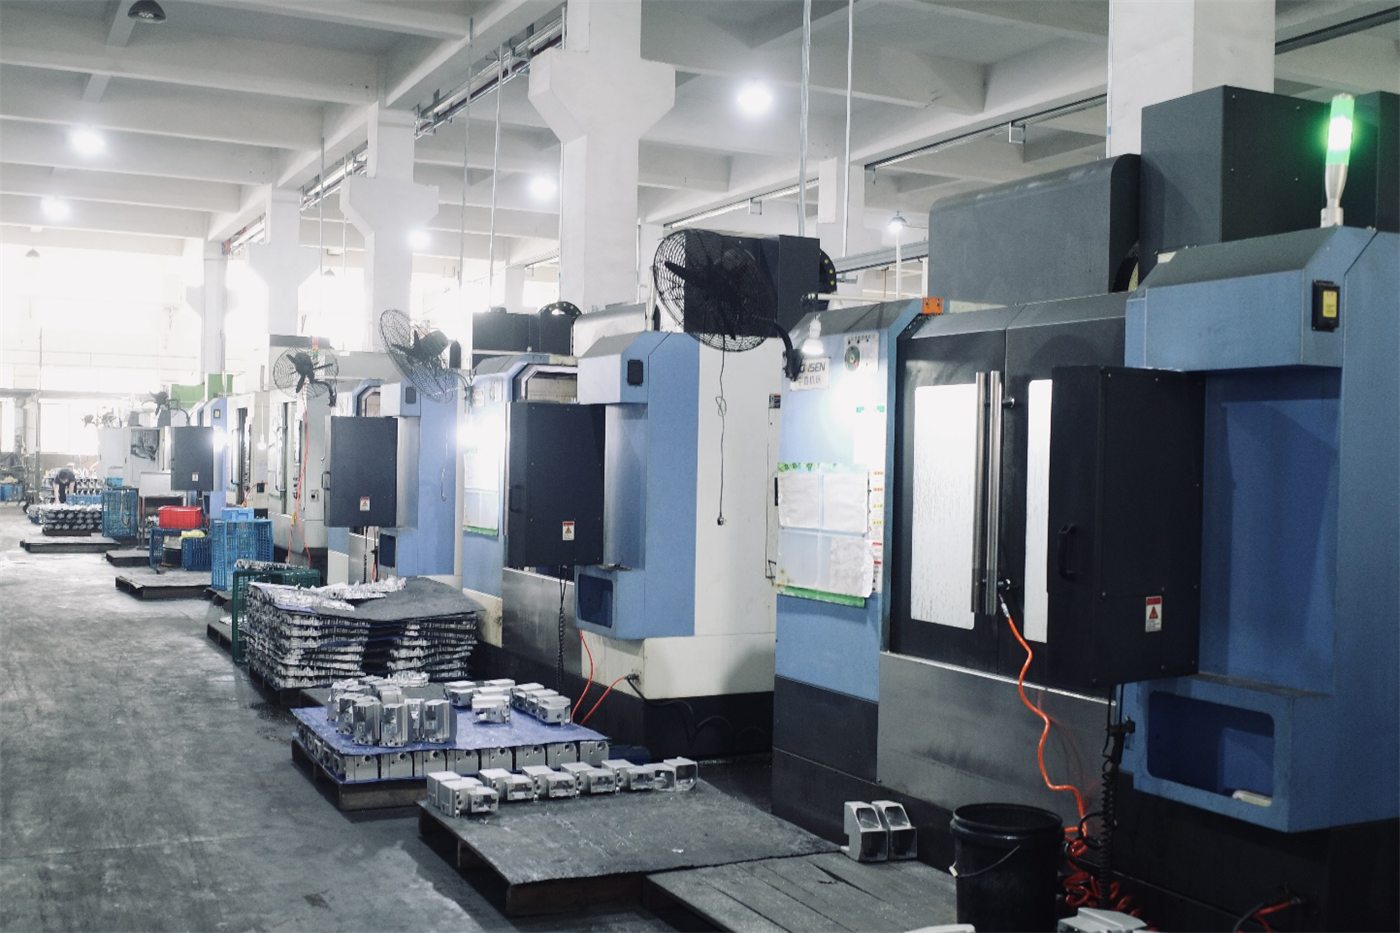
25 gravity casting machines and 10 die casters (DC280T–DC1200T), selected by geometry, wall thickness and volume. Downstream, 96 vertical drilling and milling centres and a T6 line finish the part without leaving the site. Annual capacity is 1.1 million small castings and 600,000 large castings; the catalogue now carries 170+ drawing numbers across 60+ part types.
Melting, core making, casting, heat treatment, machining and inspection are all on site, and tooling is built in-house. A revision does not queue behind an outside tool shop. Quotations separate tooling cost, sample lead time and piece price; delivery is confirmed part by part against part and tooling status.
We melt our own aluminium and cut our own moulds, and choose the process by geometry, wall thickness and volume instead of applying an expensive route to every part. Per-heat analysis, first-article CMM and X-ray sampling stop scrap before shipment. Parts for one engine platform are quoted together, avoiding multi-supplier sourcing.
Corporate film
Eighty-six seconds on the line
Melting, core making, casting, machining and inspection — shot on our own floor.
Why Guoyang
Lead time is something you control
OEM supplier audits come down to four questions: are the processes in-house, does the casting route fit the part, how fast can a revision move, and can one platform be sourced in one place.
Every process in-house
Melting, core making, casting, T6, machining and inspection all run under one roof. The four core stages — cores, casting, heat treatment and machining — are never subcontracted.
Two casting routes
25 gravity machines and 10 die casters from DC280T to DC1200T. Complex parts that need internal soundness go to gravity; thin, uniform, high-volume parts go to die casting.
Revisions move in-house
A customer drawing change is handled by our own process and tooling team, not queued behind an outside tool shop. Trial through volume stays on our schedule.
One platform, one quote
170+ drawing numbers and 60+ part types. The cylinder head, intake, cover and oil pan for the same engine can be quoted and supplied together.
Engineering & tooling
You bring the drawing. We build the process and the tool.
Thirty technical staff. Our IATF 16949 scope is manufacturing: the customer defines the part, we define the process route, the tooling and the inspection method. The drawing arrives, the manufacturability review starts before a mould is cut.
-
01
DFM & process review
Draft angles, wall thickness, gating and machining datums are checked against the customer drawing. DFM comments go back before T0.
-
02
Tooling & fixtures
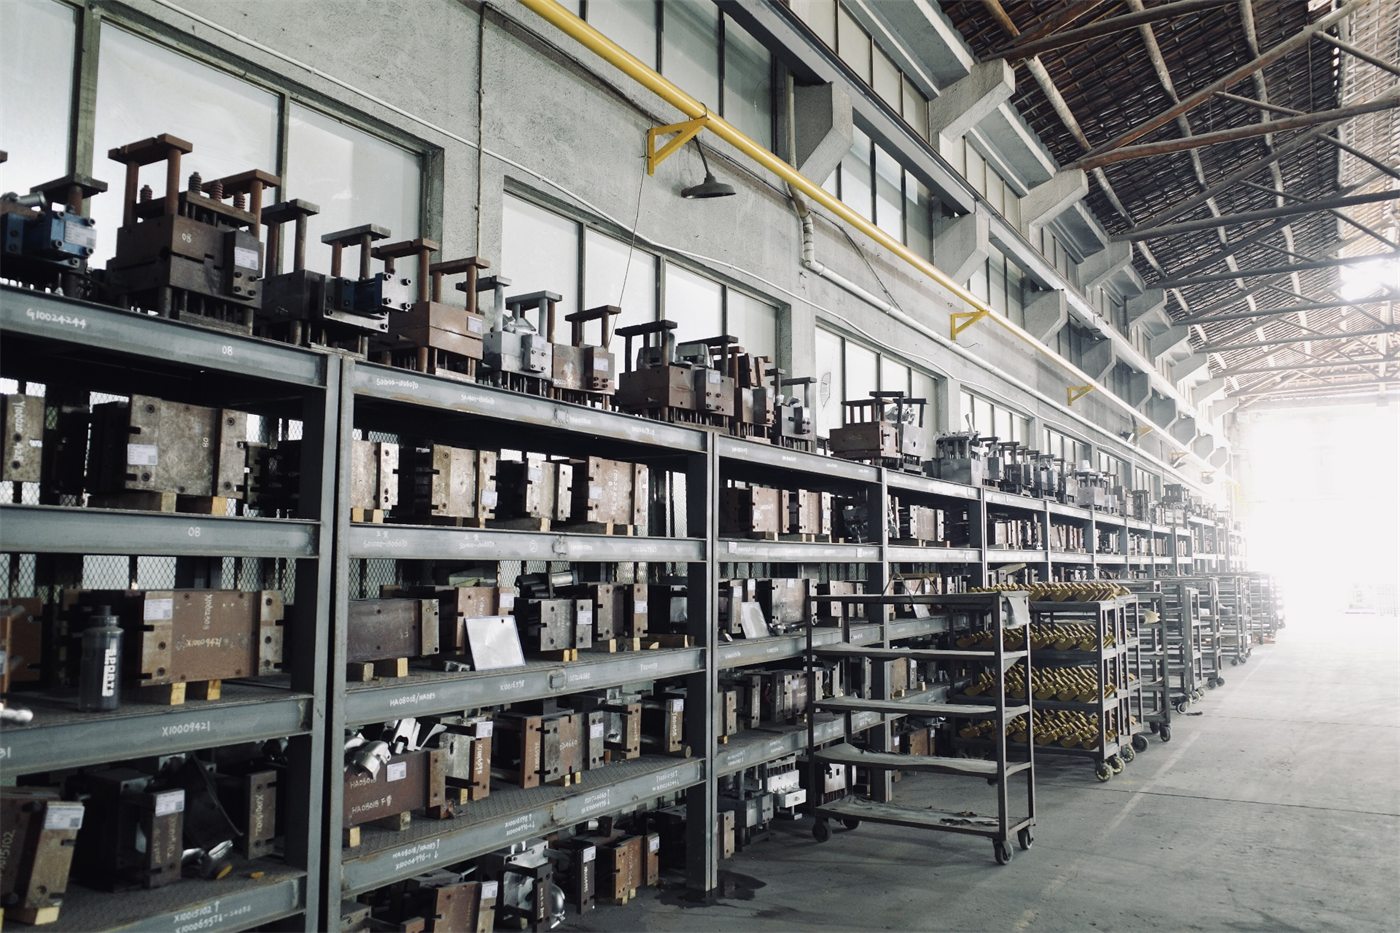
Moulds, fixtures and gauges are designed and built in-house. The mould store is racked by drawing number, with maintenance and repair on site.
-
03
Trial & first article
Trial shots, samples, dimensional and performance verification. Volume starts only after first-article approval.
-
04
APQP & PPAP
PPAP is submitted under APQP. First-pass rate was 90.7% in Jan–Aug 2026.
Products
From cylinder head to oil pan
Grouped by the name customers actually use. Each group lists lead parts, common alloys and process; the full drawing list lives on the products page.
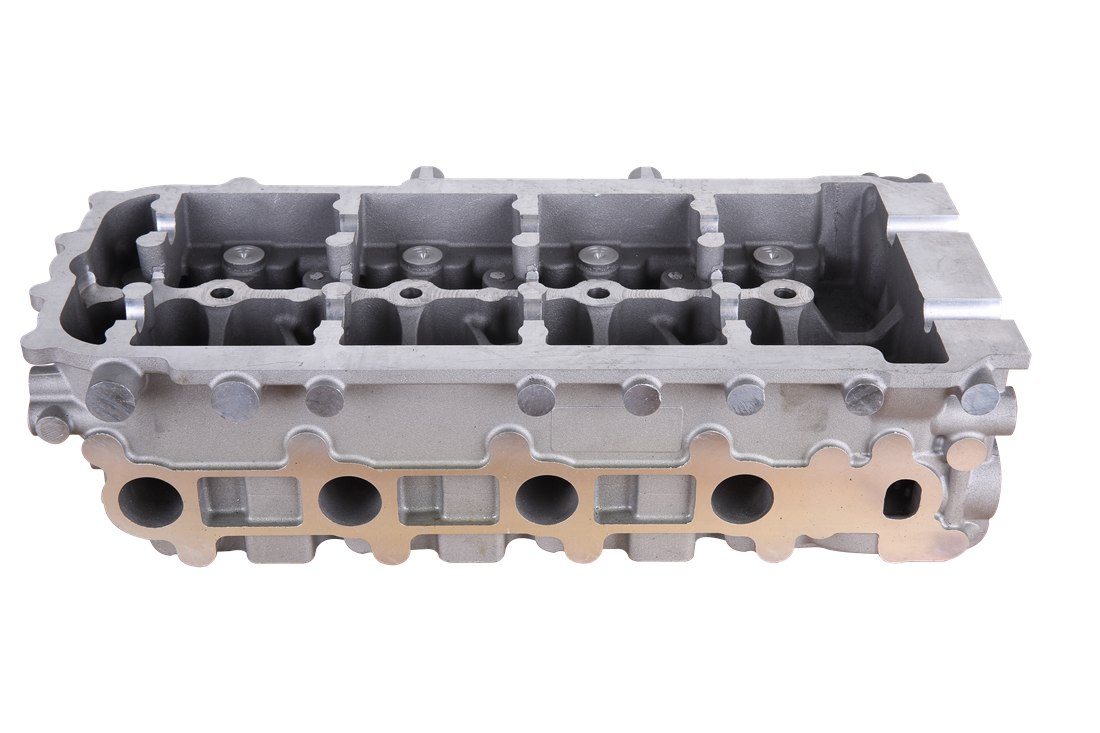
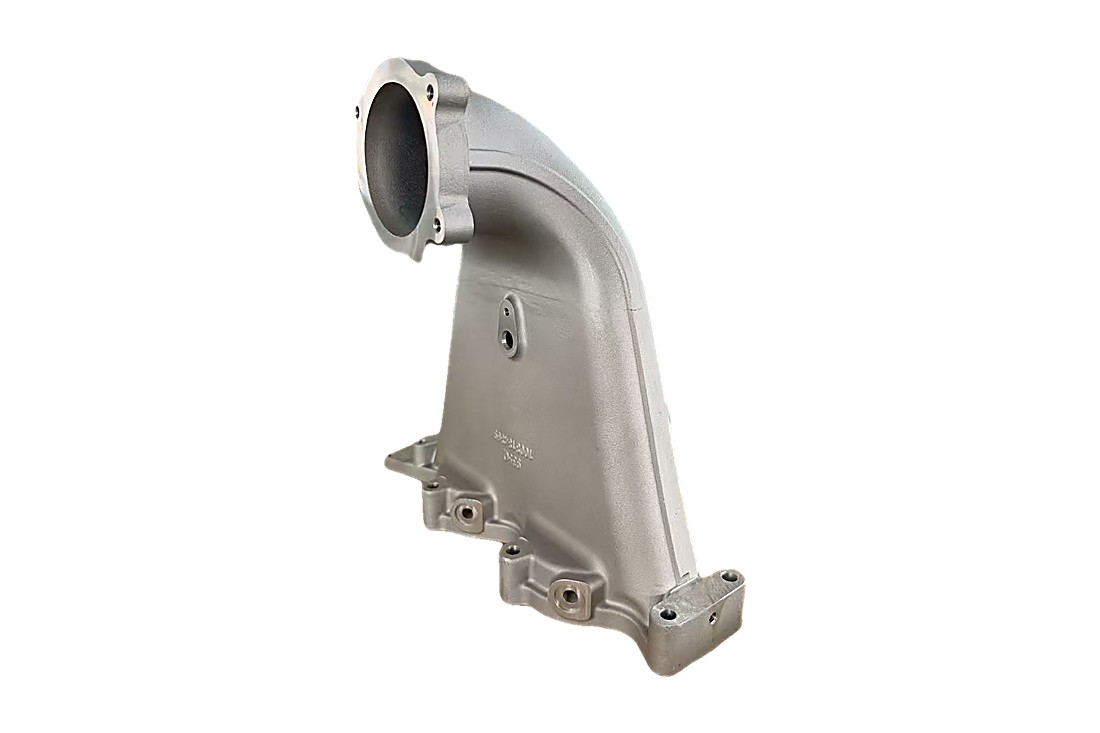
Cylinder heads & bearing caps
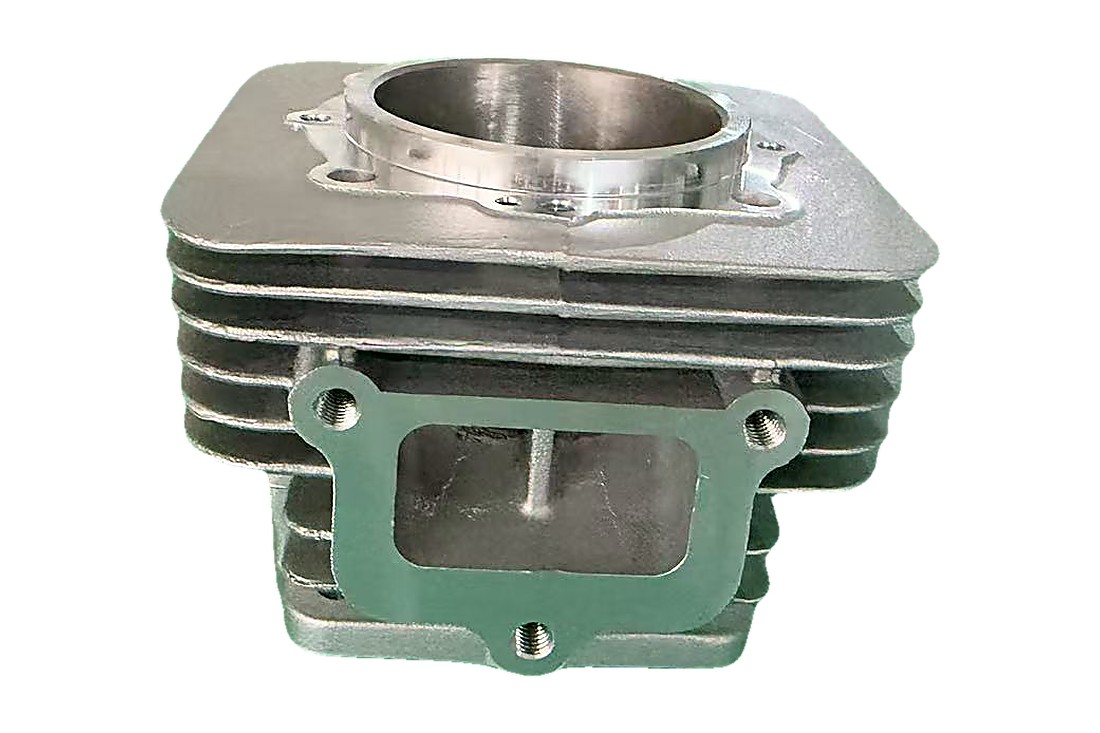
Cylinder head · camshaft bearing cap
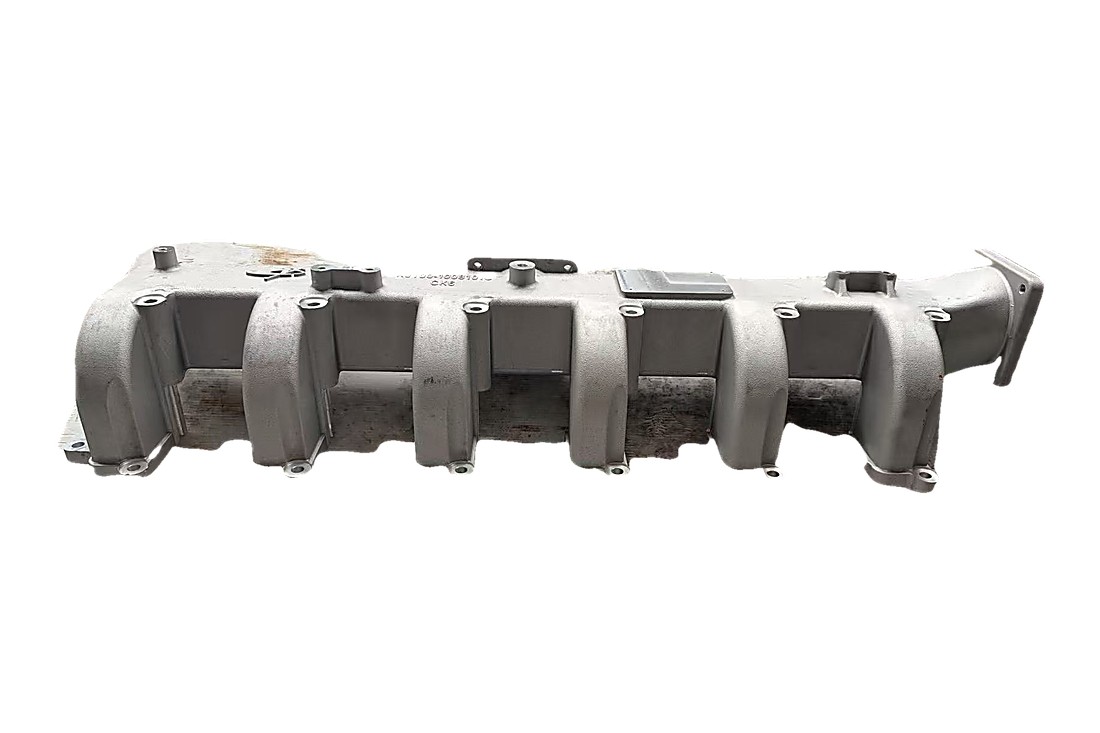
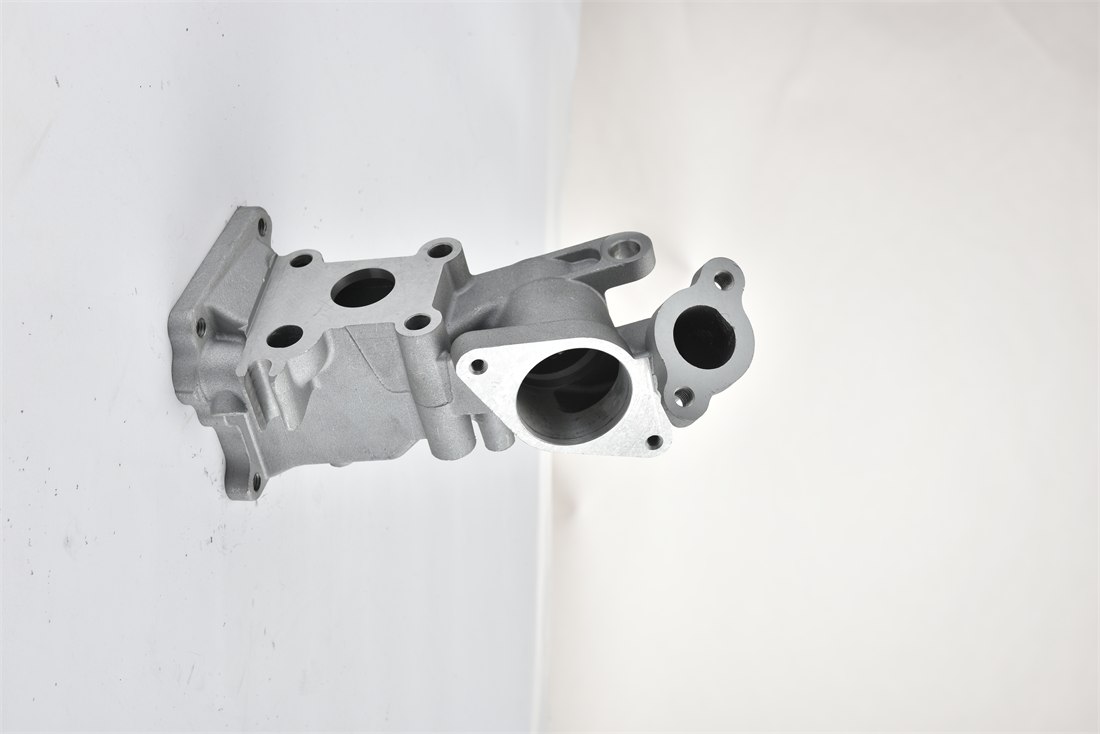
Intake, EGR & cooling
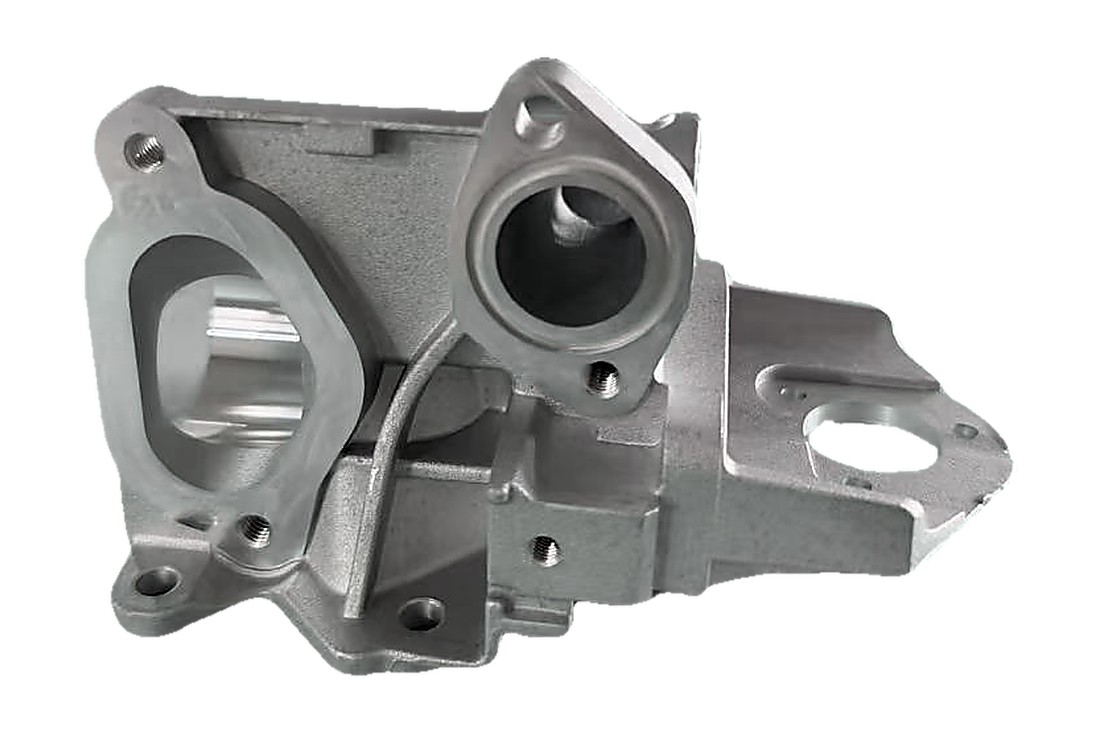
Intake manifold · intake pipe · EGR valve seat · coolant pipes
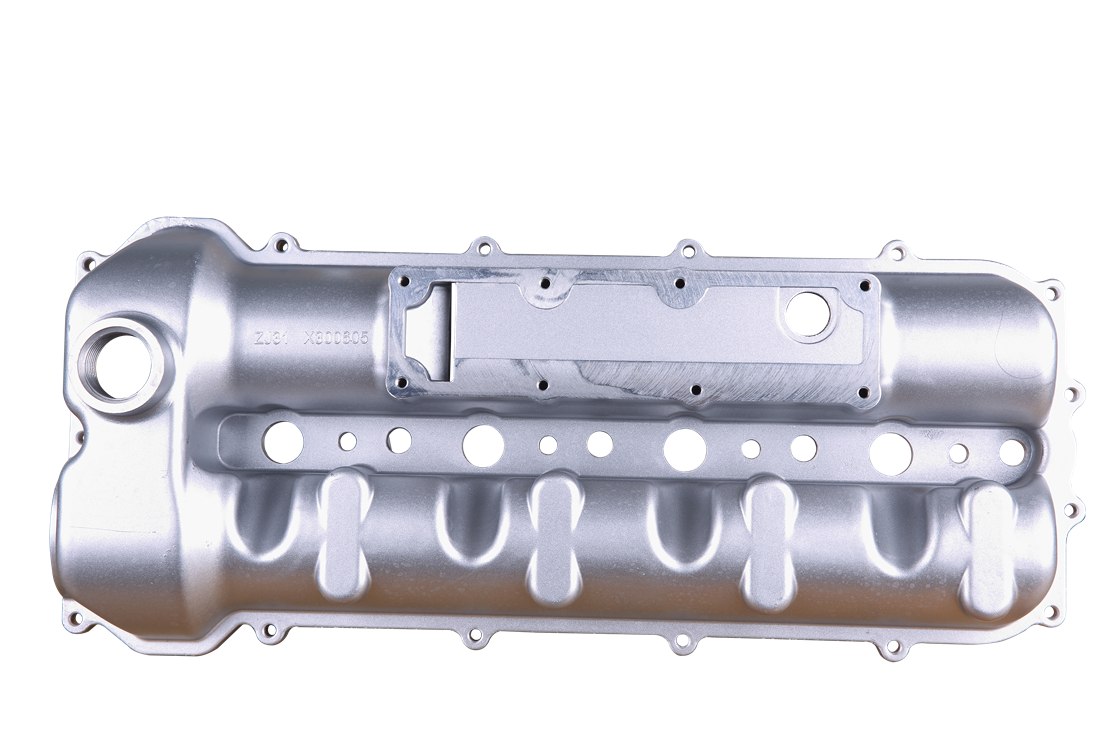
Valve covers, chain covers & gear chambers
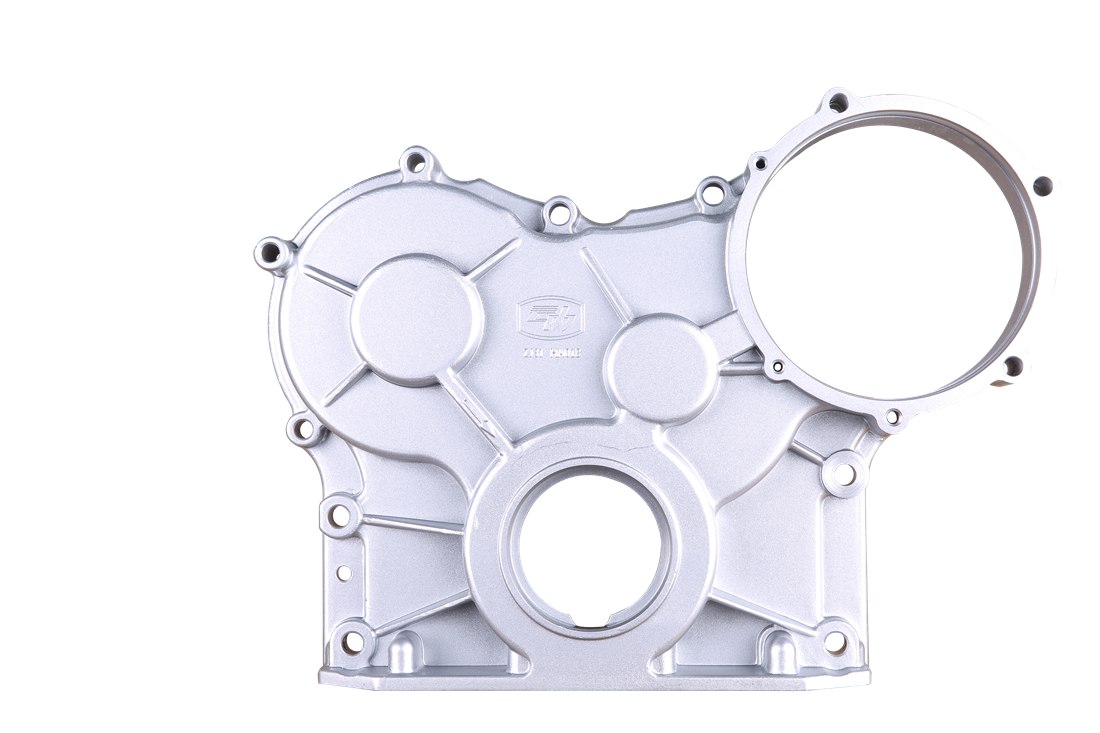
Valve cover · chain cover · gear chamber · rear gear chamber
Oil pans, strainers & pipes
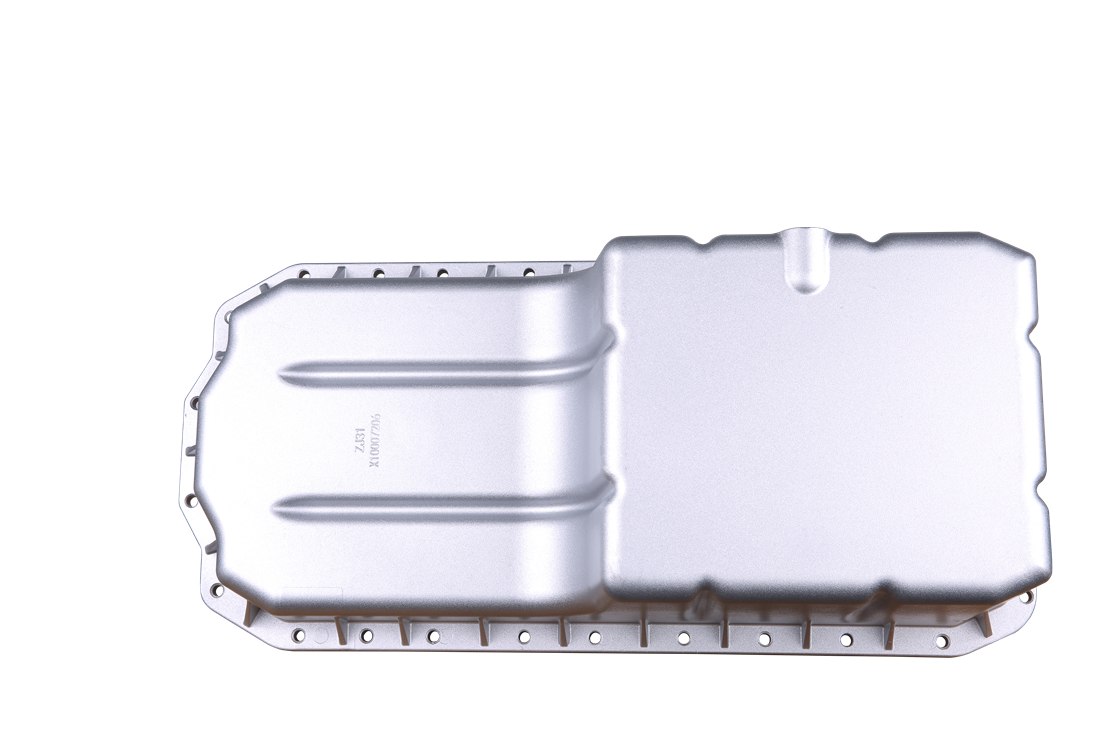
Oil pan · oil strainer assembly · heater assembly · turbo oil return pipe · dipstick tube
Brackets, housings & plastic parts
Accessory bracket · oil pump cover · vacuum pump seat · rear oil seal seat · timing cover · oil separator · filler cap
Applications
Where these parts are fitted
Guoyang supplies diesel engines and powertrains. Major customers include Weichai, Sinotruk, Yuchai, Yunnei and Xinchai, plus tier-2 assembly customers such as Fuchuang and Tianruida. The categories below group engines by downstream use; specific supply relationships are defined by customer drawings and validation.
Commercial vehicle diesel
Cylinder heads, intake manifolds, EGR seats, valve covers, gear chambers and oil pans.
Construction machinery
Intake manifolds, gear chambers, brackets and oil pans. Under continuous vibration, sealing-face flatness and thread strength are the control items.
Generator sets
Cylinder heads, intake manifolds, valve covers and oil pans. Continuous running puts the focus on dimensional stability and lot-to-lot consistency.
Agricultural machinery
Intake manifolds, intake pipes, brackets and injection-moulded parts. Many platforms, lower volume per model — lead time and cost decide.
Marine auxiliary engines
Cylinder heads, intake manifolds, coolant pipes and oil pans. High humidity and salt air raise the bar on corrosion resistance and leak-tightness.
General industrial power
Brackets, plastic parts, welded assemblies and heaters. Mostly common parts across platforms, tooled to drawing.
Note: grouped by the downstream use of the engines these parts serve; this does not imply direct supply to every end industry listed.
Equipment & process
Four process stages, all on our site
Subcontracting is where delivery and quality usually slip. Guoyang keeps core making, casting, heat treatment and machining inside the fence, so every stage is traceable to a heat and a lot. Each melt is degassed and cleaned in a refining unit; the T6 line has a solution furnace, an ageing furnace and a quench tank.
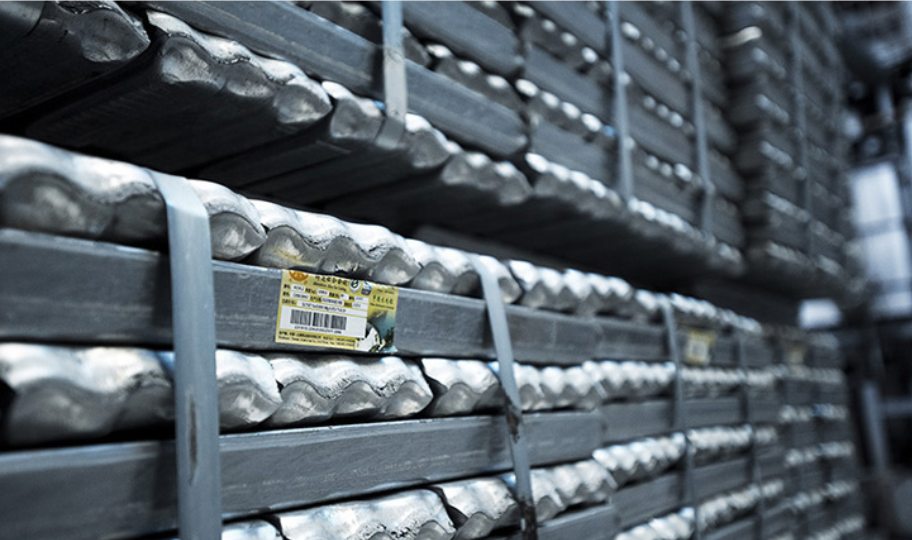
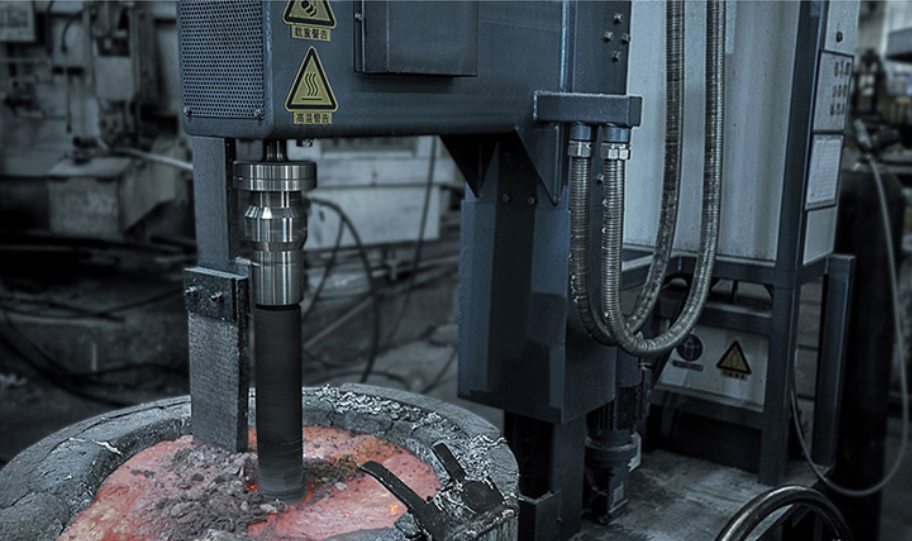
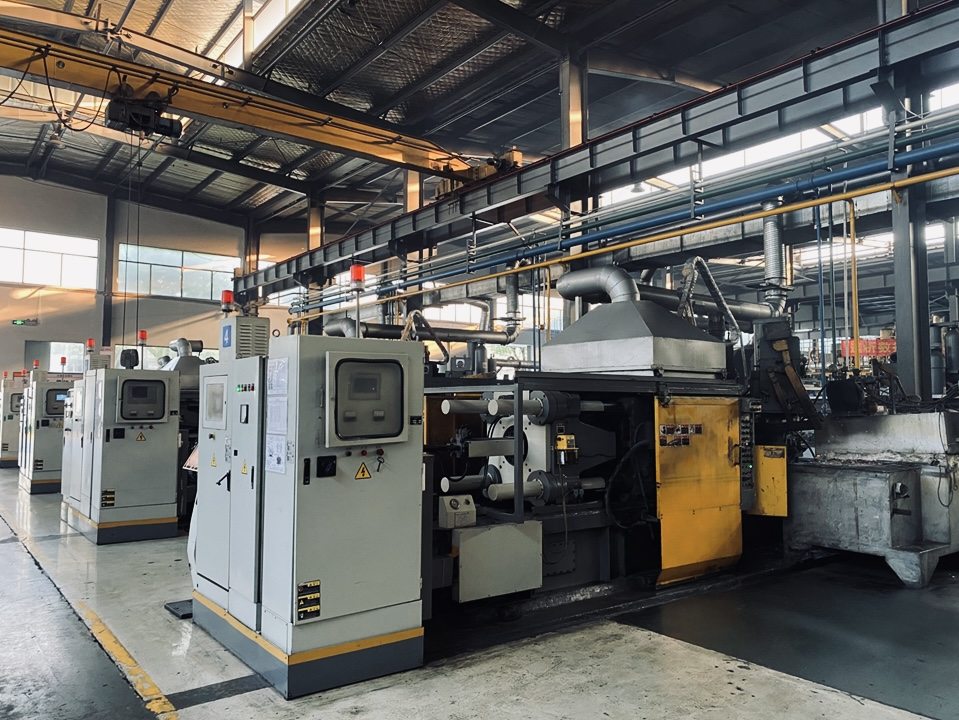
From billet to carton
The two stages in red are the ones most casting shops subcontract. Guoyang keeps them in-house.
| Selection | Gravity casting | High-pressure die casting |
|---|---|---|
| Typical parts | Cylinder heads, intake manifolds, EGR seats, valve covers — complex internal passages, pressure-tight walls | Oil pans, gear chambers, brackets, covers — uniform walls, large projected area, high volume |
| Alloys | ZL104 / ZL114A, heat-treatable to T6 | ADC12, suited to thin walls and tight as-cast dimensions |
| Process character | Risers feed shrinkage, giving high internal density; lower tooling cost suits many variants | Single-shot forming, stable dimensions, low piece cost; higher tooling investment suits volume |
| How we run it | Every heat degassed, hydrogen-tested and spectrographed; finish machining after T6 | Die temperature and shot profile controlled; shot blasting, deburring and sealing-face machining after casting |
Solution, quench and ageing on one line, to the mechanical properties the customer specifies; hardness sampled by lot.
96 vertical drilling and milling centres. Critical faces are finished in one clamping, reducing position error from re-fixturing.
Designed and built in-house. Revisions, tool repair and trials close on site, shortening the sample cycle.
How we work
A drawing in, production parts out
Six steps, each with a named deliverable. The inspection plan is agreed at the sample stage, so nobody argues about what conforming means once production starts.
Requirement
A drawing, a sample or photos. Tell us the alloy, annual volume and takt time.
Feasibility
We review casting method, parting line, machining datum and inspection plan, and send DFM notes.
Quote & tooling
The quote states tooling cost, sample lead time and piece price. No hidden line items.
Sample
Samples ship with a dimensional report, chemistry and mechanical results for your build trial.
Production
Two casting routes and 96 machining centres hold the schedule. Every heat and lot is traceable.
Packing & delivery
Preservative treatment, custom packaging, delivery to your warehouse or line side.
Quality
Every heat is tested first
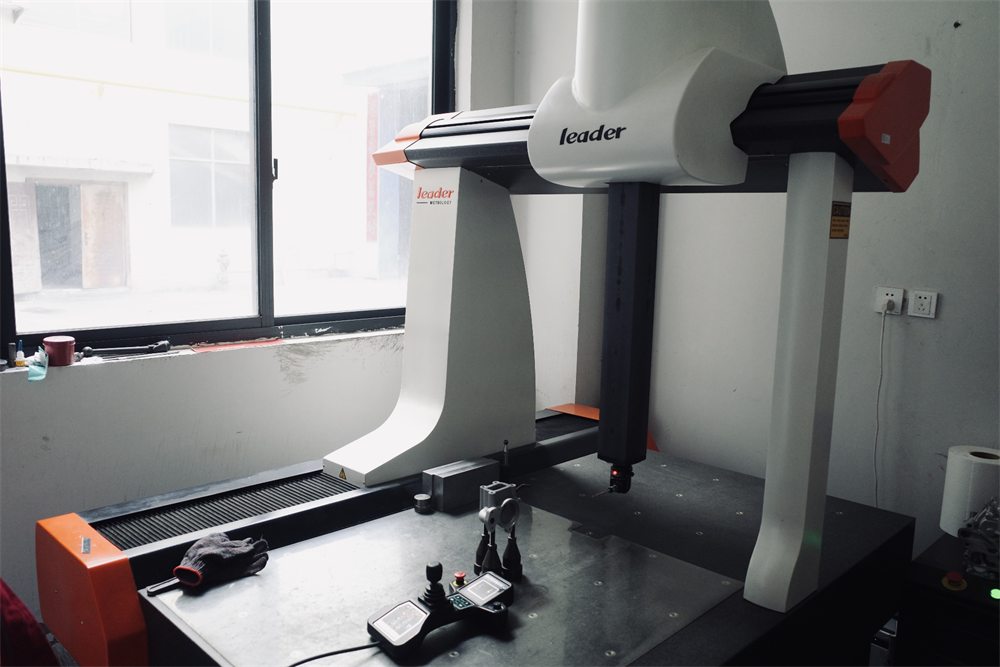
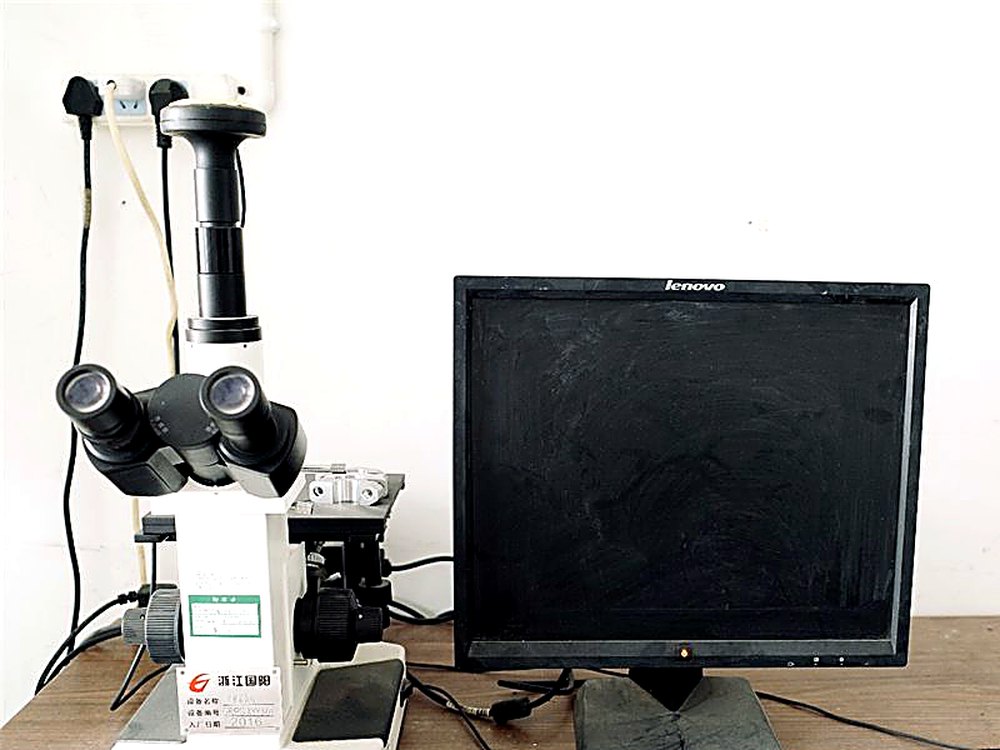
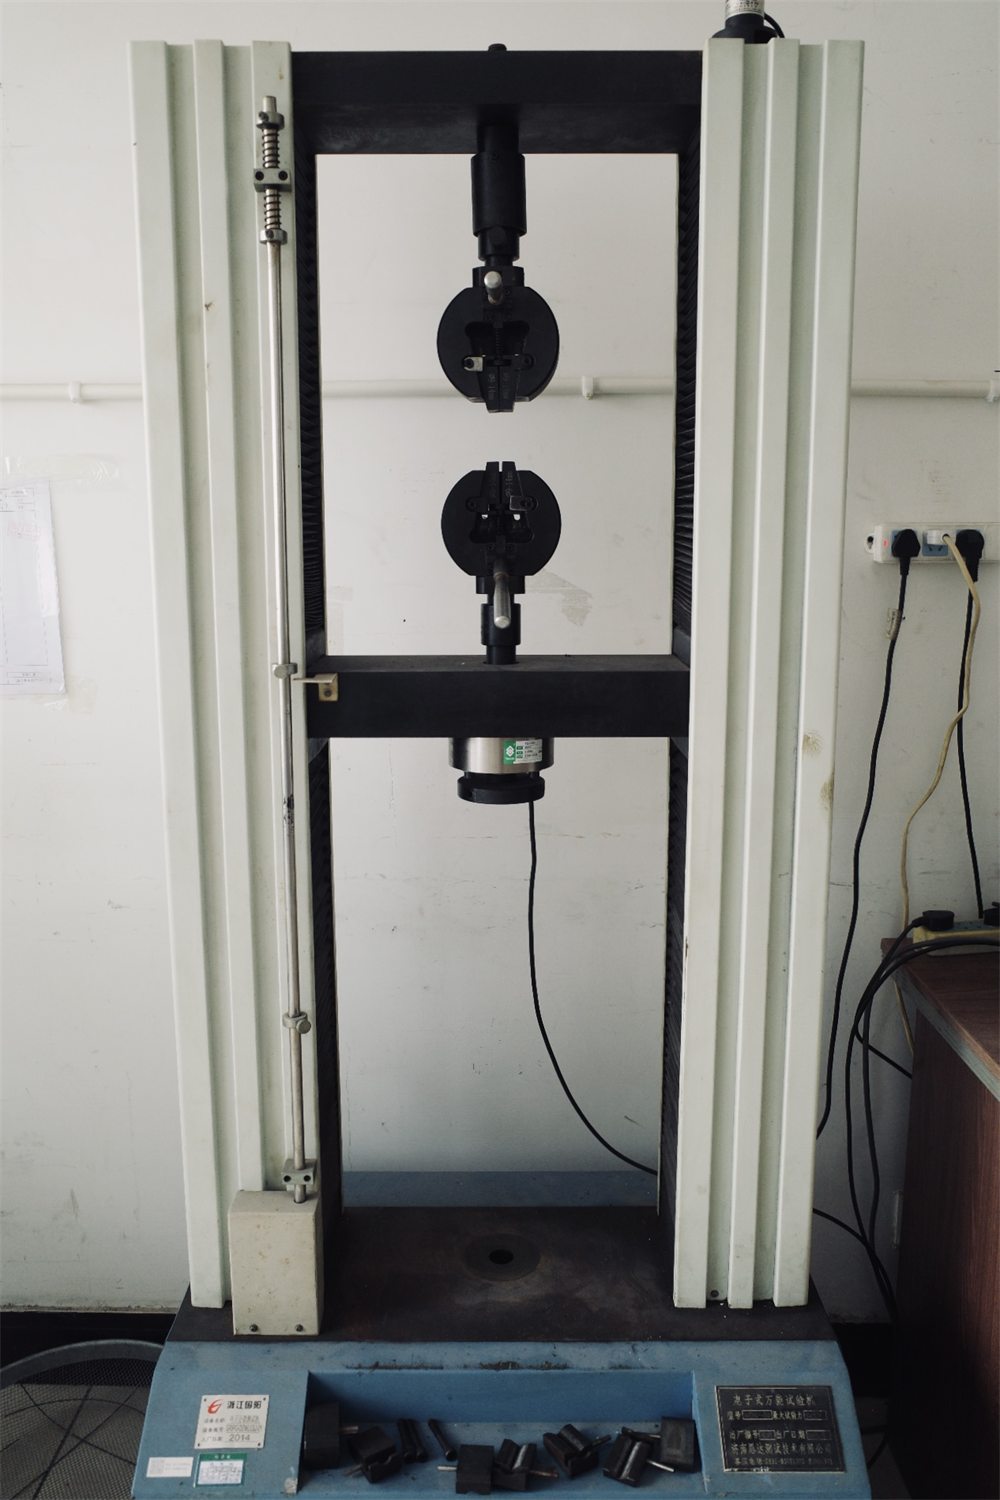
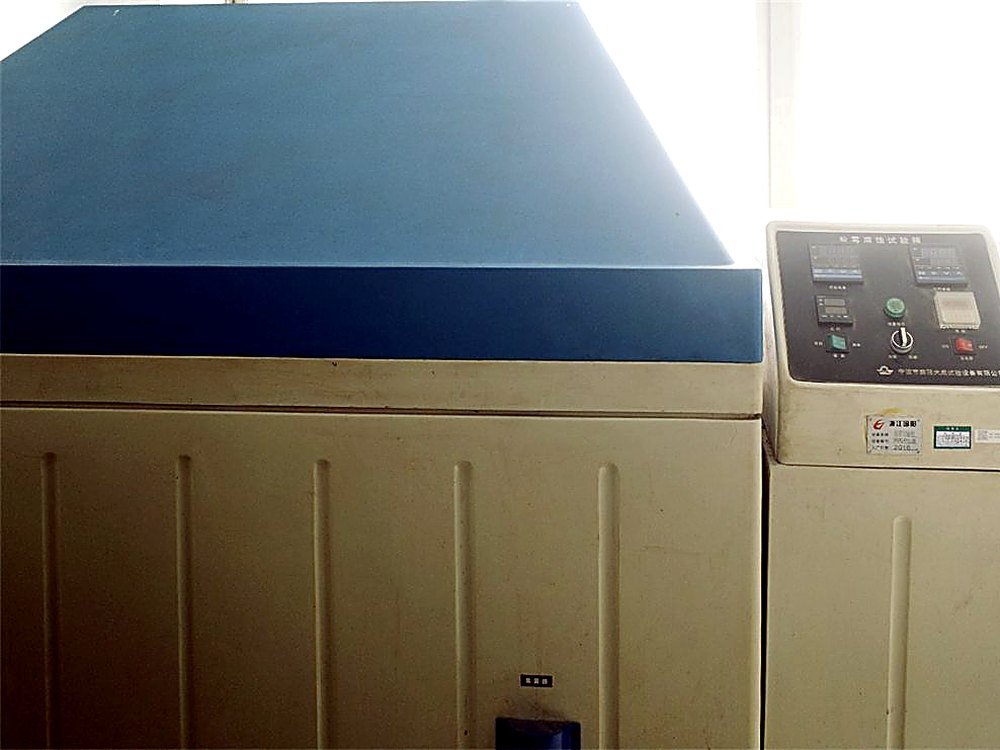
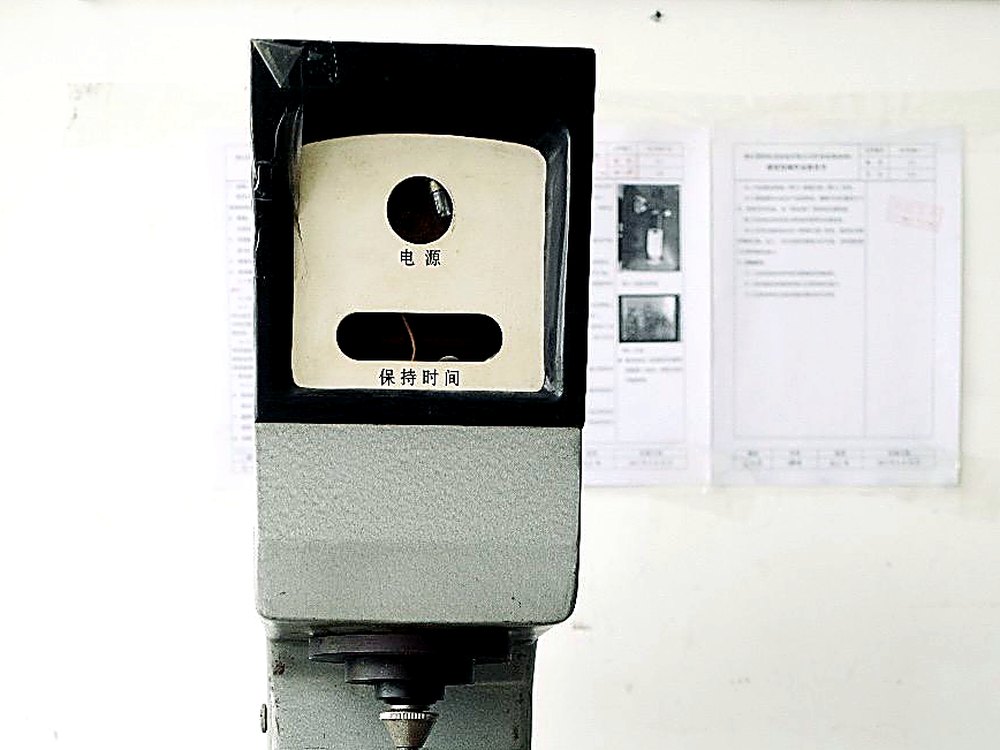
Fifteen instrument types are on site, covering chemistry, dimensions, internal defects and mechanical properties. Nothing is sent out.
Chemistry before the furnace
Every incoming alloy lot is checked on the direct-reading spectrometer. Off-spec material does not reach the melting floor.
Every heat is watched
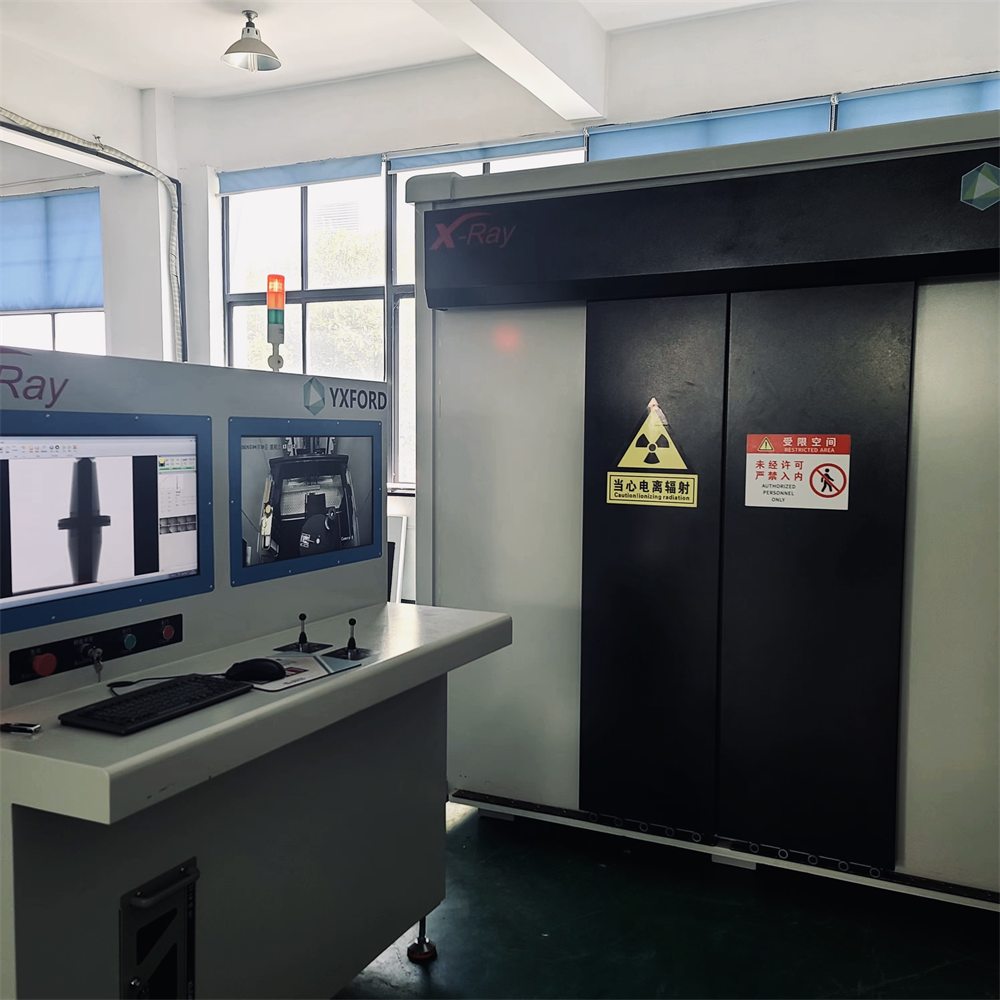
Hydrogen, degassing and pouring temperature are recorded per heat; first articles are confirmed on the CMM and X-ray sampled by lot.
Accepted against the drawing
Leak, hardness, mechanical properties and salt spray follow the customer drawing and control plan. Reports travel with the lot.
Back to the heat
Heat, lot, machine and operator records are linked, so a suspect part can be traced to its raw material and process parameters.
| Instrument | Model / brand |
|---|---|
| Direct-reading spectrometer | MAX LMD04 · Shanghai Spectro; plus VL-4000 · Wuxi Chuangxiang |
| Coordinate measuring machine | NC8107 · Qingdao Leiton |
| X-ray inspection | XT7600 · Yifangda |
| Hydrogen content tester | VF053 · Zhejiang Wanfeng |
| Universal testing machine | WDW-50 · Jinan Sida |
| Brinell hardness tester | HB-3000 · Laizhou Dechuan |
| Leeb hardness tester | XH960 · Hangzhou Shiyi · 2 units |
| Metallurgical microscope | PRJX41 · Shandong Zhongke Purui |
| Surface roughness tester | XH260 · Shanghai Xinhuan |
| Ultrasonic thickness gauge | ST-200 · Yongkang Siwei · 2 units |
| Salt spray chamber | YWX/Q-1000 · Ningbo Benyang Dacheng |
| Cleanliness tester | BH-500 · Ningbo Benyang Dacheng |
| Coated sand tester | YJ48S · Sanmen Sante · 2 units |
| Pneumatic gauge | LZA-ML · Yongkang Lantian |
| Granite inspection table | 1000 × 1000 mm |
Quality targets, measured
Jan–Aug 2026 · internal figures, not third-party audited
Quality policy: customer satisfaction and zero defects; controlled processes and continuous improvement.
System scope: IATF 16949:2016, NQA certificate T86992 / IATF 0502960,
valid 28 Feb 2024 – 27 Feb 2027; manufacture of injection-moulded parts and aluminium
castings (product design excluded), covering Buildings 1 and 2, No. 178 Xueyuan North Road.
Certifications & records
Every certificate can be checked
Each item below is backed by a certificate or a public record. Customer names and marks identify supply relationships only and remain the property of their owners.
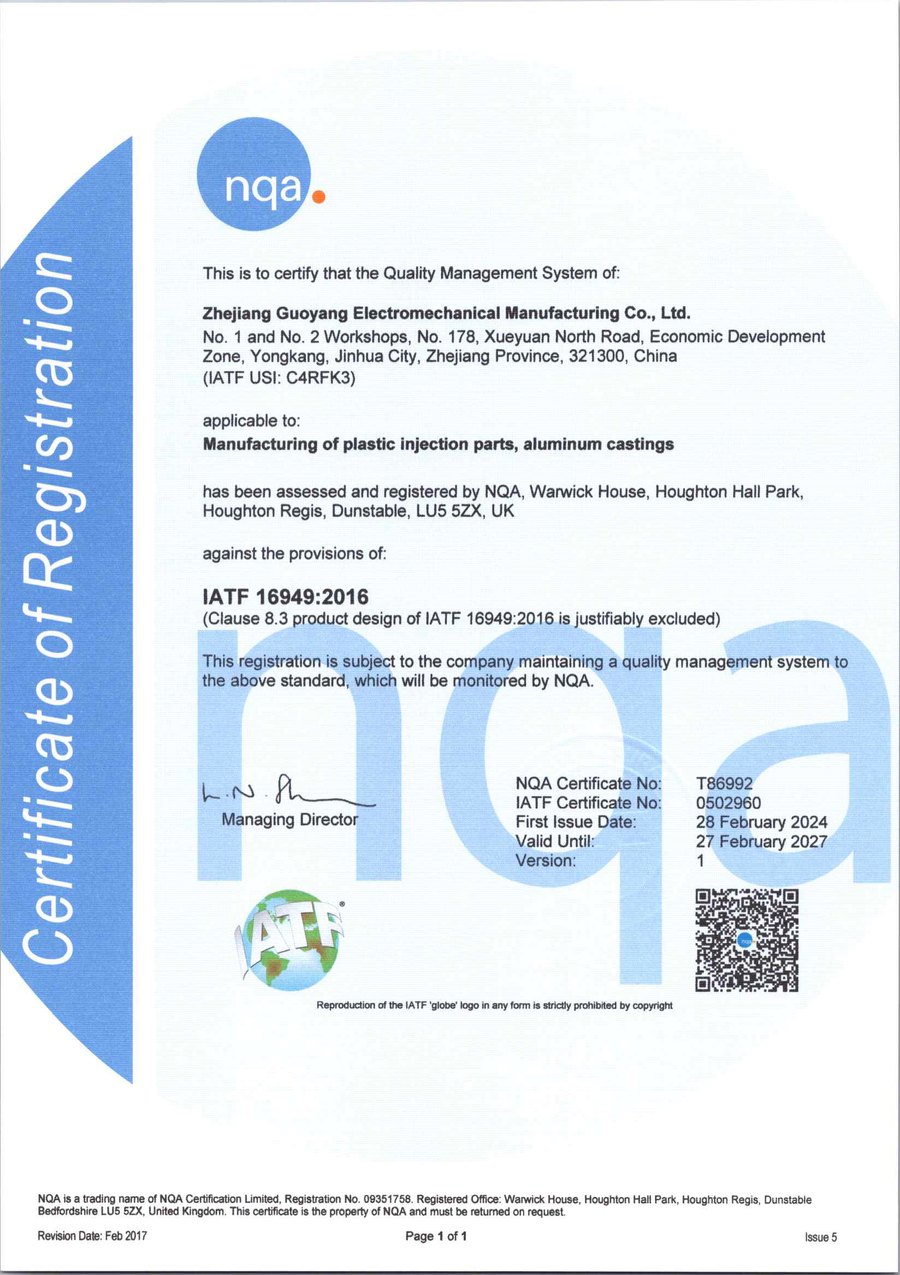
IATF 16949:2016
NQA certificate T86992 · IATF 0502960; valid 28 Feb 2024 – 27 Feb 2027; scope: manufacture of injection-moulded parts and aluminium castings (product design excluded), covering Buildings 1 and 2.
Continuous certification · 2021 → 2027
The 2021 certificate 0391201 ran to 23 March 2024; the current certificate 0502960 took effect on 28 February 2024 and runs to February 2027.
Zhejiang High-Tech Enterprise
Recognised as a Zhejiang Province high-tech enterprise by the provincial high-tech enterprise accreditation authority.
No. 3 plant completed
25,049 m² of additional factory floor space.
333 kWp rooftop solar
Completed on-site solar project with 333 kWp installed capacity.
OEM supplier award
Annual excellent-supplier award from a major Chinese diesel-engine manufacturer.
Business registration
Unified Social Credit Code 91330700769607709H; registered capital RMB 41.2 million; incorporated 6 December 2004.
Invention patent · intelligent aluminium-bar casting machine
ZL 2020 1 1232947.7; granted 2 November 2021; patentee: Zhejiang Guoyang Electromechanical Manufacturing Co., Ltd.
Utility model · die-cleaning device
ZL 2020 2 2574536.8; granted 19 November 2021; patentee: Zhejiang Guoyang Electromechanical Manufacturing Co., Ltd.
Business registration and patents can be checked in the National Enterprise Credit Information Publicity System and the China National Intellectual Property Administration database; customer audit reports and other originals are available on request.
Major customers
Engine OEMs
Tier-2 assembly customers: Fuchuang, Tianruida and others.
Some customers are shown; names and marks identify supply relationships only and remain the property of their respective owners.
Knowledge
Aluminium casting notes
Six short notes on process, alloy, heat treatment, defects and machining. Compiled from public technical material and industry standards; the customer drawing and technical agreement always govern.
Gravity casting or HPDC? Start with wall thickness, volume and heat treatment
Neither process is better. Wall thickness, annual volume, T6 and welding requirements usually decide before the tool is cut.
T6 heat treatment: what it changes, and why ordinary die castings cannot take it
Solution, quench and ageing change more than hardness: ductility, dimensional stability and cost all move.
ADC12 vs A356: two casting alloys that are not interchangeable
One is made for die casting; the other can be strengthened by heat treatment. The wrong choice carries the process and cost with it.
Gas porosity and shrinkage: where internal defects come from and how to find them
One comes from gas, the other from insufficient feeding. They look different on an X-ray and need different fixes.
Machining allowance: why more is not safer
Too little leaves black skin and defects. Too much adds cost, exposes porosity and increases distortion risk.
Lightweighting commercial vehicles: where aluminium castings fit, and where they do not
Replacing iron with aluminium is not an all-or-nothing move. Temperature, stiffness, cost and recycling set the boundary.
Contact
Send the drawing
Tell us the part, alloy, annual volume and whether tooling is needed. We will come back with a process route, tooling lead time and piece price.
Zhejiang Guoyang Electromechanical Manufacturing Co., Ltd.
178 Xueyuan North Road, Yongkang Economic Development Zone,
Yongkang, Zhejiang, China
Contact Mr. Ying
Tel +86 158 6793 6599
Fax +86 579 8751 6780
Email guoyangjishu@cnzjgy.com
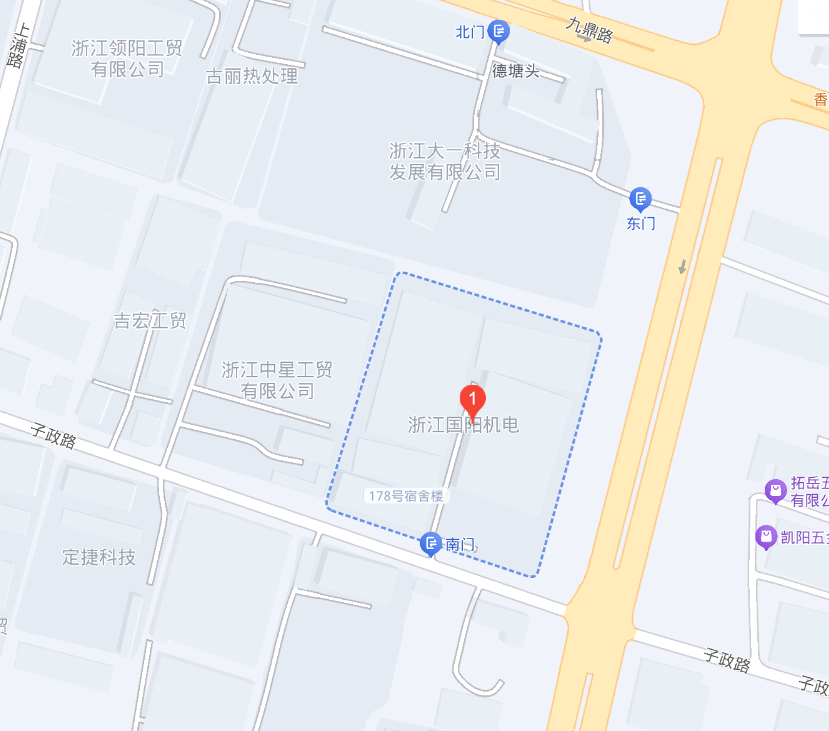 Plant location · open in Baidu Maps →