Sales +86 158 6793 6599 guoyangjishu@cnzjgy.com No. 178 Xueyuan North Rd, Yongkang, Zhejiang, China
Zhejiang Guoyang Electromechanical Manufacturing Co., Ltd. EN / 中文

Home/ Products/Plastic components

Plastic components, our second product line

Engine covers, timing covers, oil separators and oil filler caps. Injection-moulded in PP / PA66, with metal inserts, ultrasonic welding and sub-assembly where the drawing calls for it. Injection-moulded parts fall within our IATF 16949:2016 scope and share the same quality system and lot traceability as the aluminium parts.

05Representative parts 02Material systems 02Moulding & joining 01Quality system

Products / Plastic components

Appearance parts that do a job

Plastic is not an accessory to the aluminium line. Covers and timing covers have to hold their assembly dimensions and seal faces; the oil separator has to keep its internal passages clean, oil-resistant and sealed; the filler cap has to fit its seat. Visible surfaces are colour-matched to the customer's standard, and production parts are first-off approved, patrol-inspected and checked before dispatch.

Material follows the drawing: PP for general covers and guards, PA66 where higher strength, oil resistance or temperature resistance is required. Grade, colour and additives are set by the customer drawing.

Material
PP / PA66
Selected per drawing; colour to customer standard
Moulding
Injection
Appearance, assembly dimensions and draft controlled
Assembly
Inserts / welding
Metal inserts, ultrasonic welding and sub-assembly
Quality system
IATF 16949
Moulded parts in scope (product design excluded)

Part range / Representative parts

Five representative parts

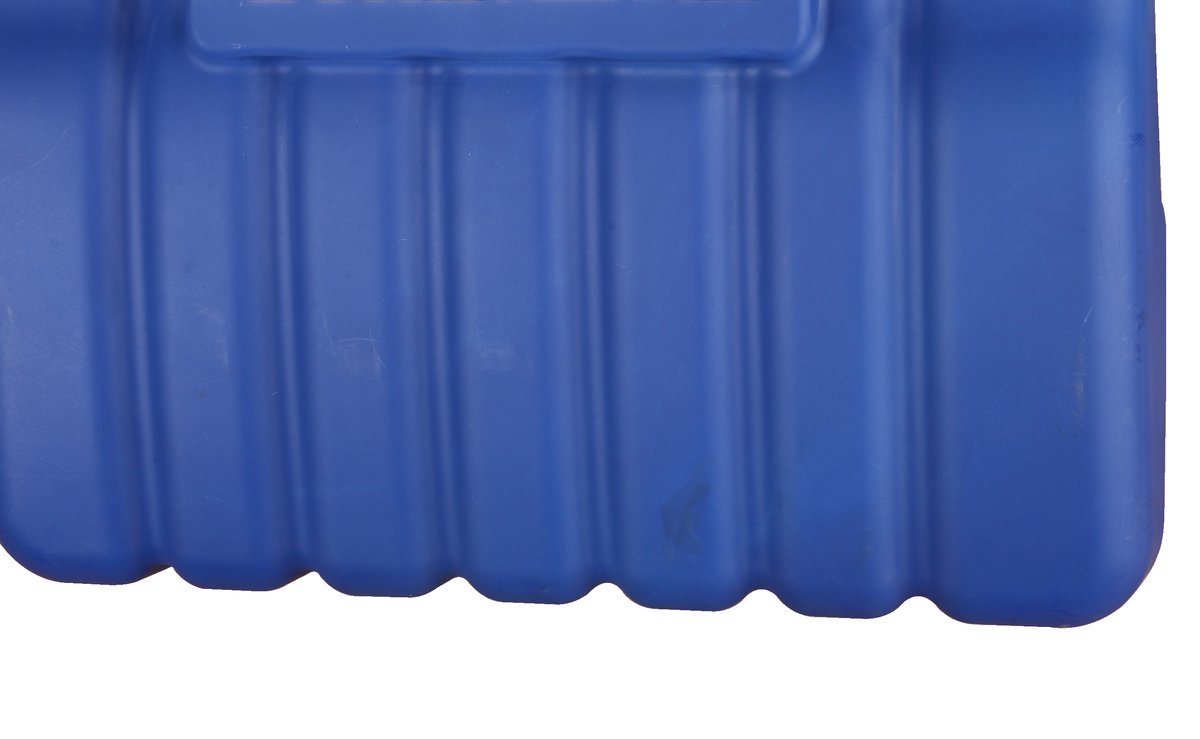
Photos show production parts. The engine cover is shown as a rib detail only; customer marks have been cropped from the other photos. Confirm display rights before publishing.

P-01 Engine cover rib detail Rib and wall detail · customer mark not shown

P-01 / ENGINE COVER

Engine cover

ENGINE COVER

Visible cover over the cylinder head. Deep draw, thin walls and dense ribbing make flow balance, packing and draft angle critical. The visible surface is colour-matched to the customer standard; no visible sink, weld line, flash or colour variation is accepted, and mounting holes must align with neighbouring parts.

Material
PP / PA66 (per drawing)
Process
Injection moulding
Controlled
Appearance & colour · assembly dimensions · sink and warpage
Fitment
Multiple engines
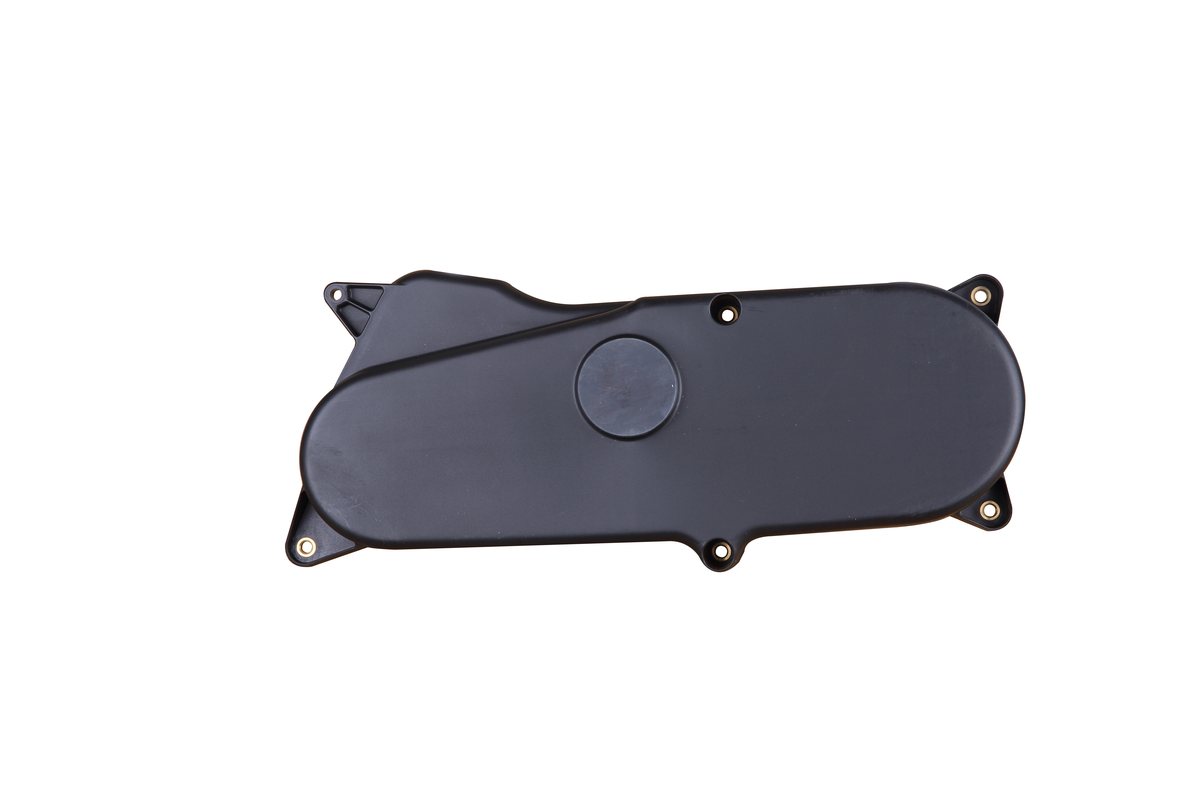
P-02 Front timing cover

P-02 / FRONT TIMING COVER

Front timing cover

FRONT TIMING COVER

Thin-walled, large flat cover at the front of the timing gear chamber, with metal inserts in the mounting holes. Seal-face flatness, hole position and insert pull-out strength are the main controls; parts are checked on a fixture after moulding.

Material
PP / PA66 (per drawing)
Process
Injection + inserts
Controlled
Flatness · hole position · insert strength
Fitment
Multiple engines
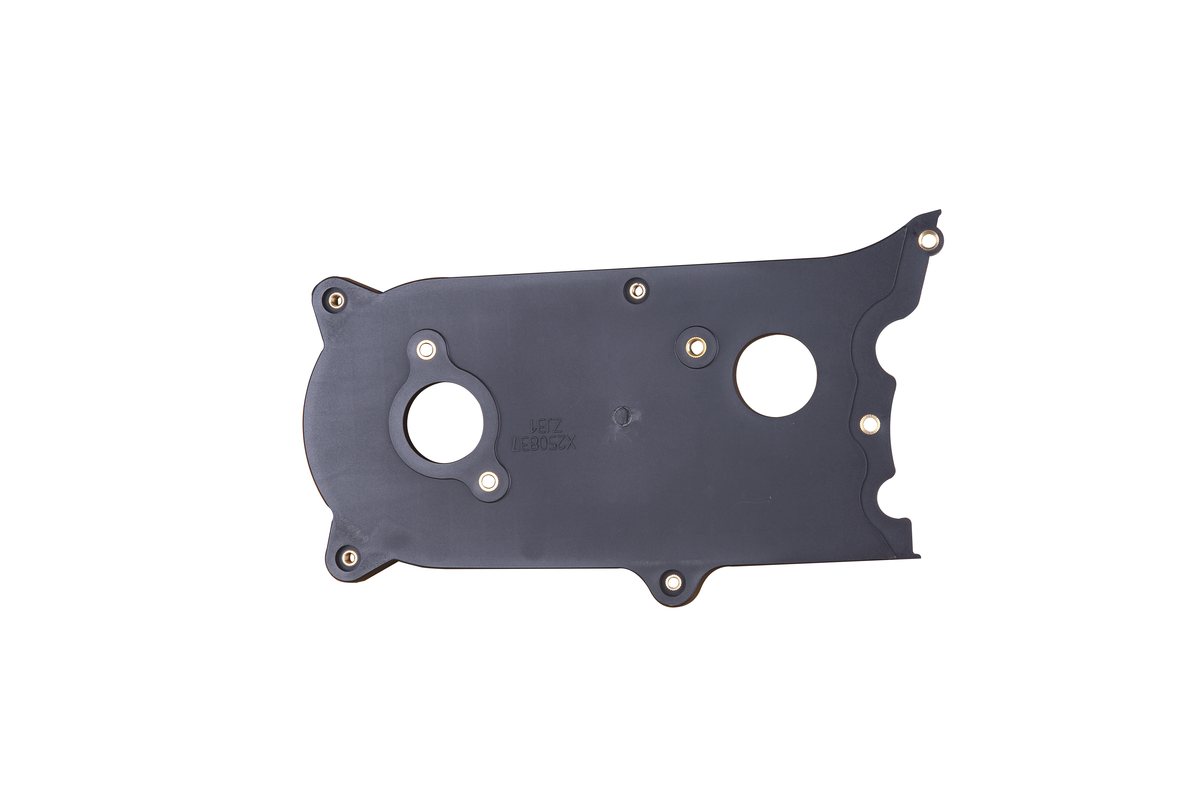
P-03 Rear timing cover

P-03 / REAR TIMING COVER

Rear timing cover

REAR TIMING COVER

Shaft openings and clearance cut-outs; hole position and flatness determine how the cover seats against the block. First-off approval and patrol checks follow the customer drawing, with shaft-bore alignment and seal-face contact as key items.

Material
PP / PA66 (per drawing)
Process
Injection + inserts
Controlled
Shaft-bore position · flatness · seal face
Fitment
Multiple engines
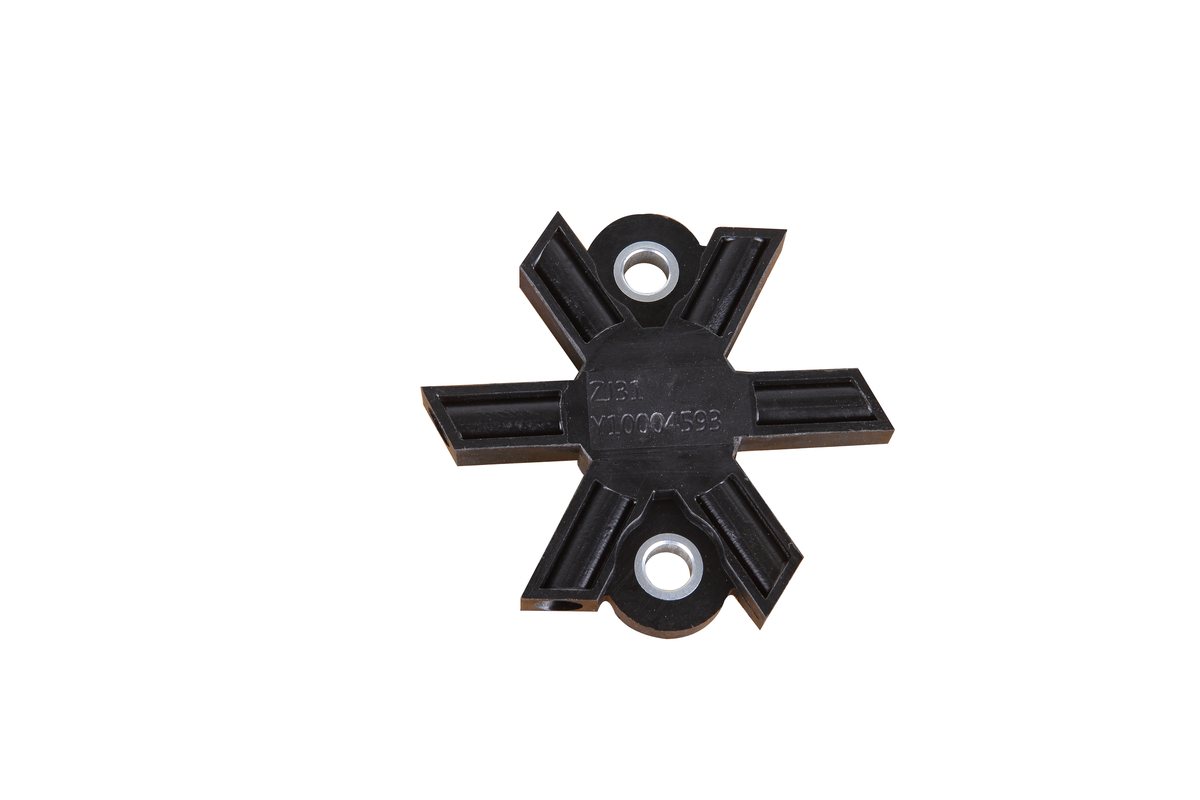
P-04 Oil separator

P-04 / OIL SEPARATOR

Oil separator

OIL SEPARATOR

Four reinforced arms around a central separation chamber, with metal inserts in the mounting holes. Internal passage cleanliness, oil resistance and seal faces are the main controls; assembly is verified when supplied as a sub-assembly.

Material
PA66 (per drawing)
Process
Injection + assembly
Controlled
Sealing · oil resistance · passage cleanliness
Fitment
Per drawing
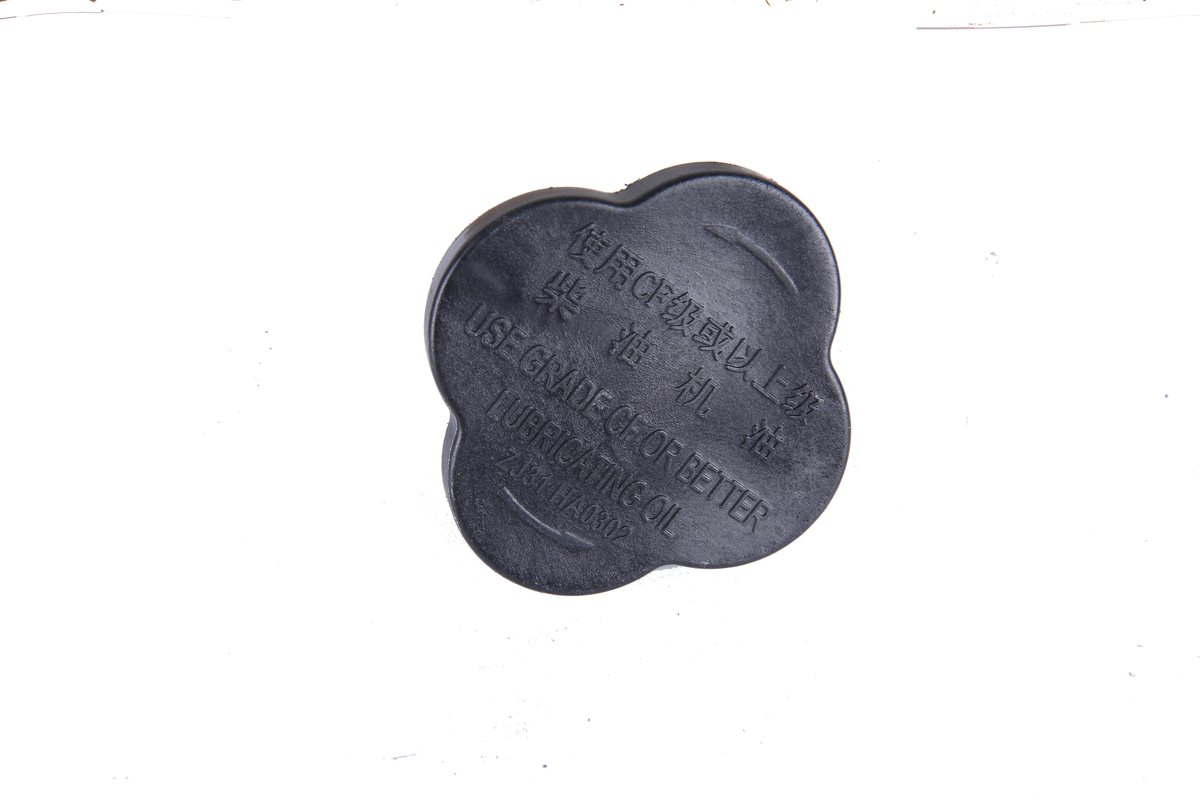
P-05 Oil filler cap

P-05 / OIL FILLER CAP

Oil filler cap

OIL FILLER CAP

Sealing cap matched to the filler neck, with customer-specified instruction text moulded into the top. Seal-ring fit, oil resistance and opening torque are the main controls; colour follows the customer standard.

Material
PA66 / PP (per drawing)
Process
Injection + assembly
Controlled
Sealing · oil resistance · opening torque
Fitment
Per drawing

Process / From pellet to assembly

From pellet to assembly

Process outline only; the actual route follows the part drawing and customer requirements. Parts requiring welding or sub-assembly add those steps after moulding.

01

Material check

Grade, colour, additives and lot checked to drawing; regrind ratio controlled.

02

Injection moulding

Mould, melt, packing and cycle per process card; first-off appearance and dimensions.

03

Trim / deflash

Gate, flash and drag marks removed; visible surfaces checked to limit samples.

04

Inserts / welding / assembly

Metal inserts, ultrasonic welding and seal fitting verified to the assembly drawing.

05

Inspection / packing

Appearance, colour, assembly dimensions and sealing sampled to the inspection plan.

Equipment note: injection-moulding machine tonnage, count and installation years are still being confirmed against the asset register. This page does not list models yet; they will be added to Equipment & Capacity once verified.

Quality / What we control

What we control on moulded parts

Appearance, dimensions, sealing and material are controlled separately. Inspection items and frequency are agreed at sample stage and then run to the production inspection plan.

Appearance

Appearance & colour

Compared with the customer colour standard and limit samples; sink, weld line, flash, drag marks and colour deviation controlled.

Dimension

Assembly dimensions

Mounting holes, flatness, clips and insert positions checked on fixtures or a CMM; full first-off dimensional report.

Sealing

Sealing & oil resistance

Oil separator and filler cap verified to drawing for sealing and media compatibility; sub-assembly air test where required.

Traceability

Material & lot

PP / PA66 grade, colour lot, moulding parameters and inspection records archived by lot and traceable to raw-material batch.

IATF 16949:2016 · certificate scope

Manufacture of injection-moulded parts and aluminium castings (product design excluded).

NQA certificate T86992 / IATF 0502960, valid 28 Feb 2024 to 27 Feb 2027. Plastics and aluminium share the same system documentation, supplier management and lot traceability.

Public disclosure

This page lists only parts that can be verified from the product photo library and existing records. Customer names, OEM marks and customer part numbers in product photos are not shown until written permission is held; production status, material grade and engine fitment must be confirmed item by item before publication.

Send plastic drawings with the aluminium ones

We can quote moulded parts in the same project as castings. Please state material grade, colour and annual volume, and whether the part needs inserts, welding or sub-assembly.